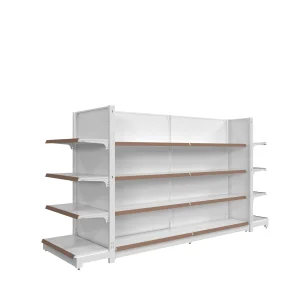
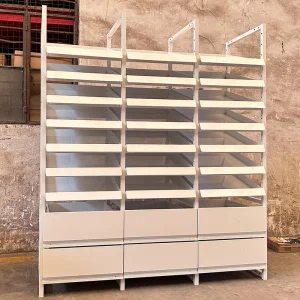
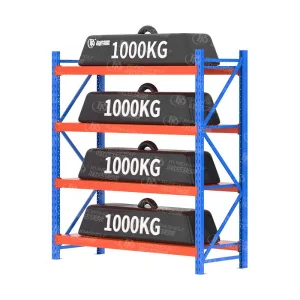
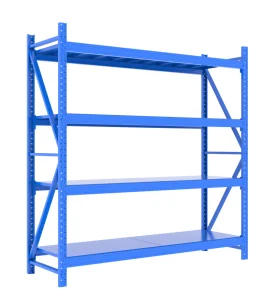
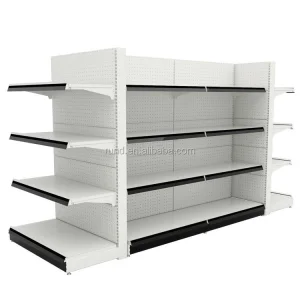
Ningbo CrownRacking Intelligent Warehouse Tech Co., Ltd. has been pioneering warehouse solutions since 2018. Operating out of a 46,500 m² modern production complex, we produce an annual export revenue of $42,000,000. Our operational success is backed by 5 years of international trade experience and 8 years of industry dedicated leadership.
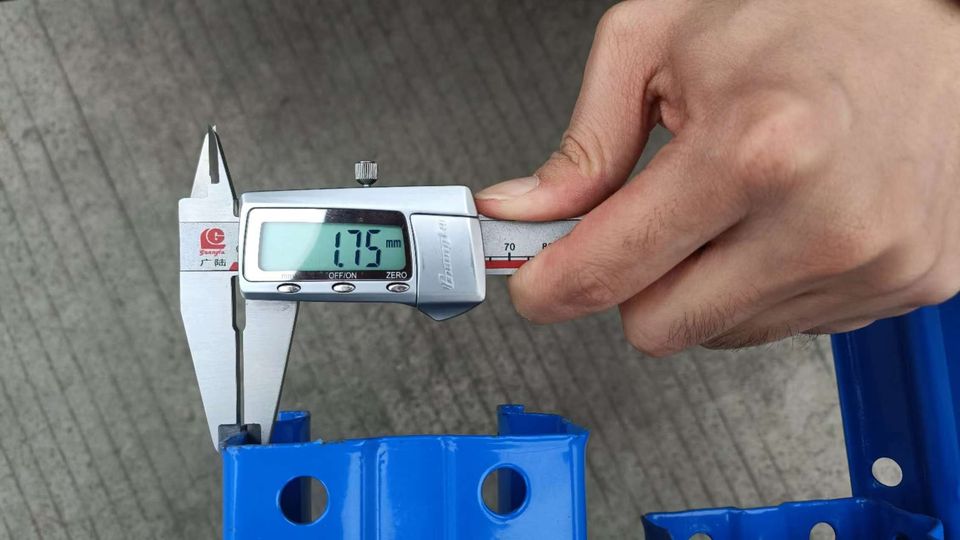
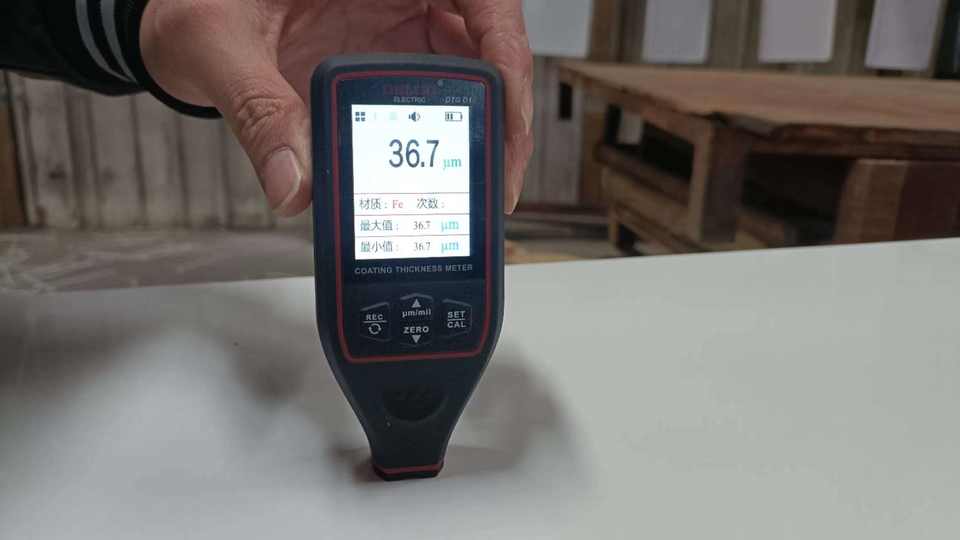
We guarantee structural durability through rigorous Full-Cycle In-Line & Final Stress Load Inspection, employing Laser Coordinate Measuring & Coating Thickness Verification managed by 62 QC staff members. With a Factory Direct Exporter with Global Turnkey Project Services trade background, our primary markets cover Australia, Northern Europe, and North America. We are supported by 1,850 supply chain partners, serving major client types including pharmaceutical distribution networks, retail logistics parks, and heavy machinery warehouses.
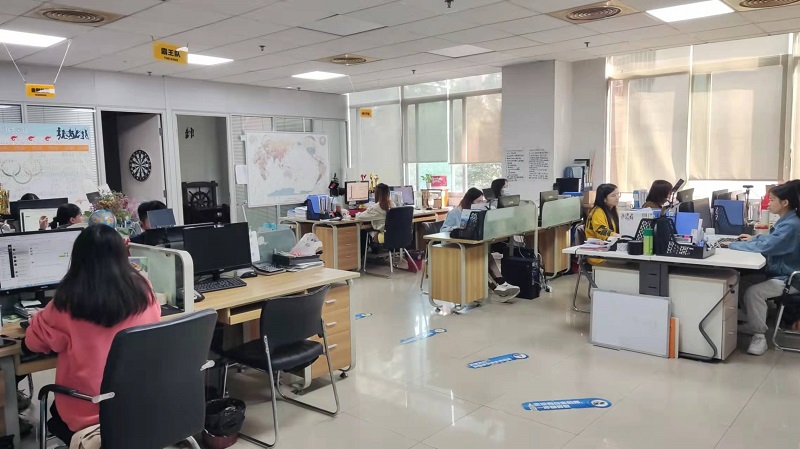
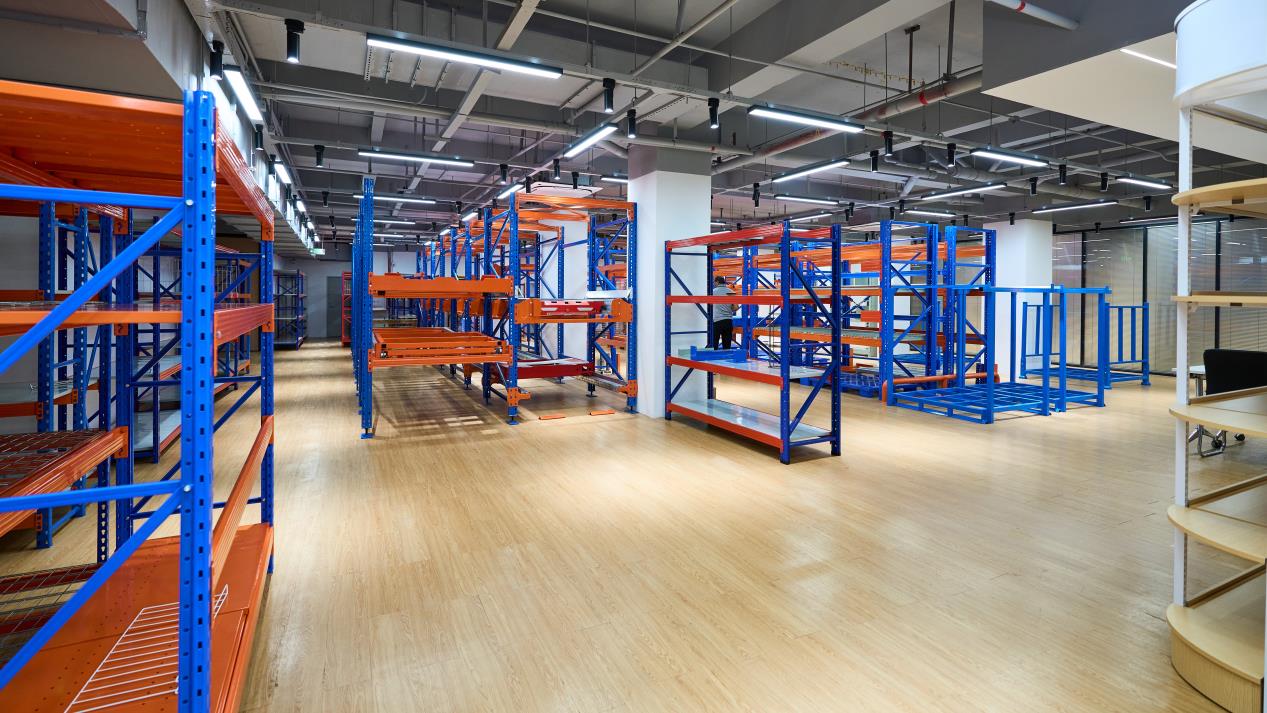
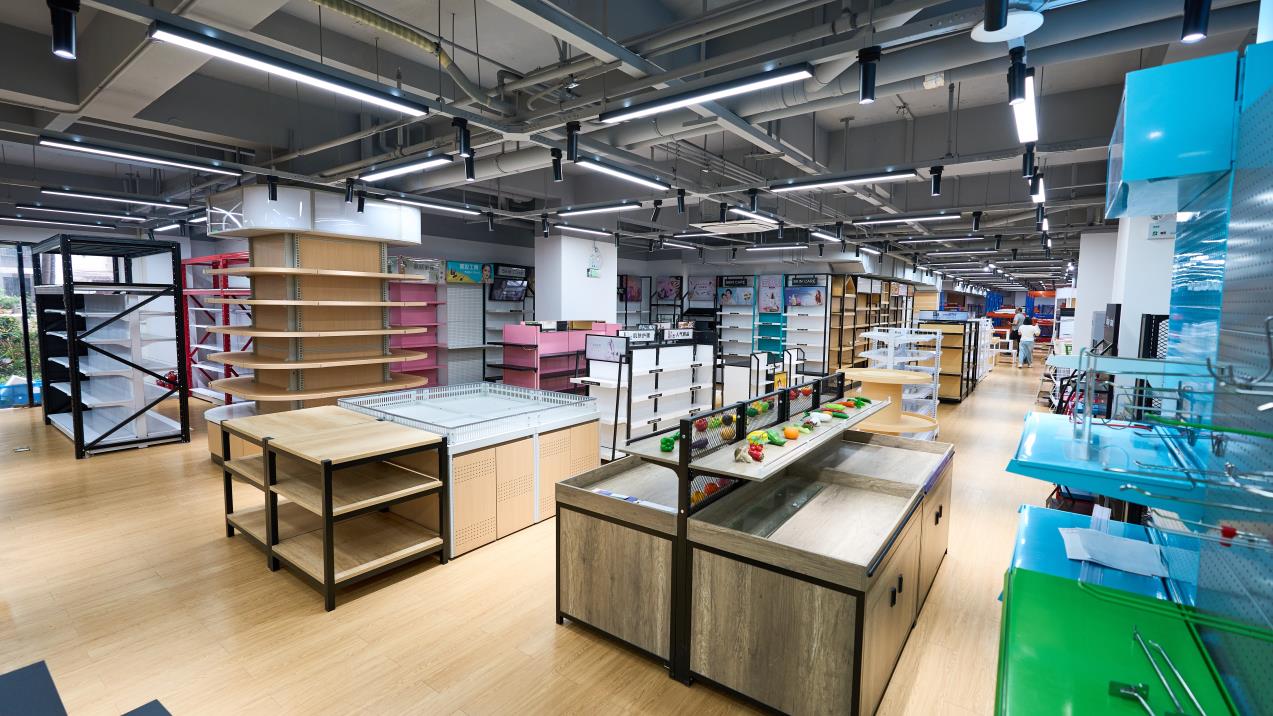
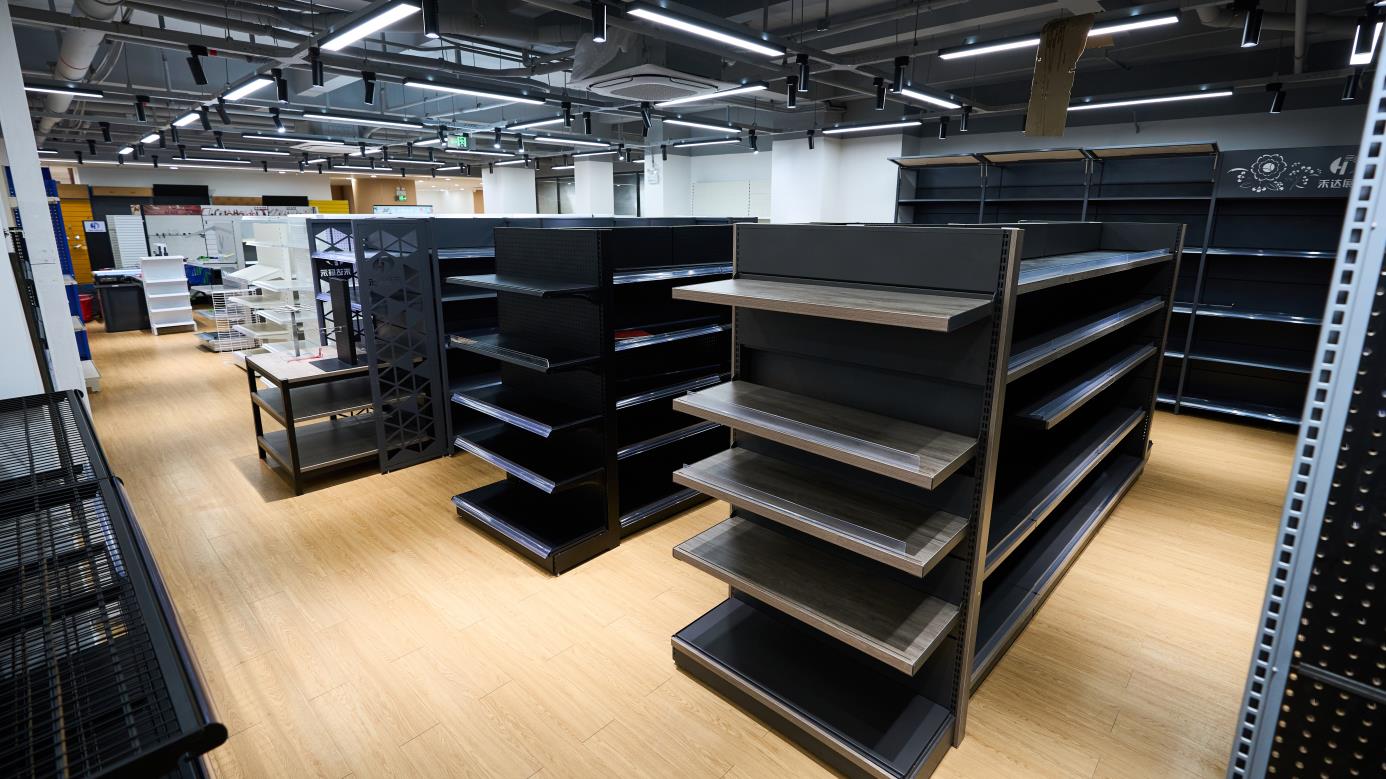
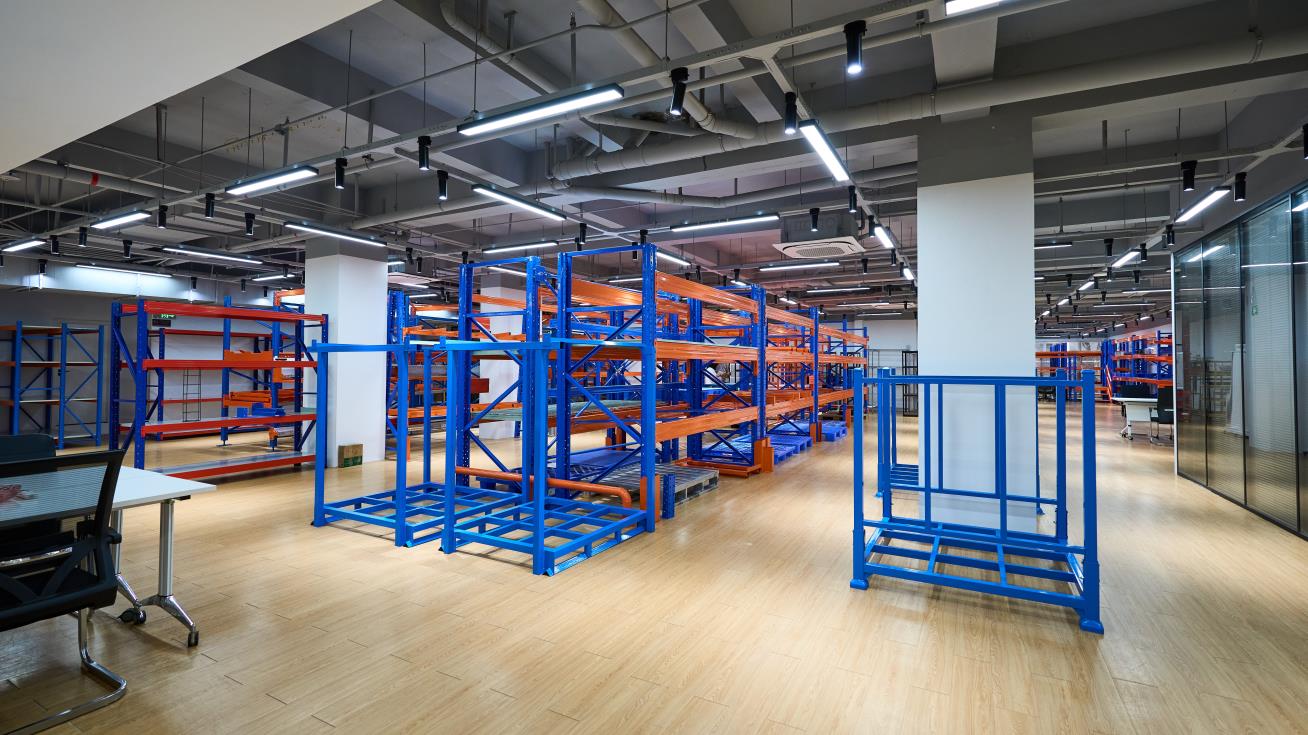
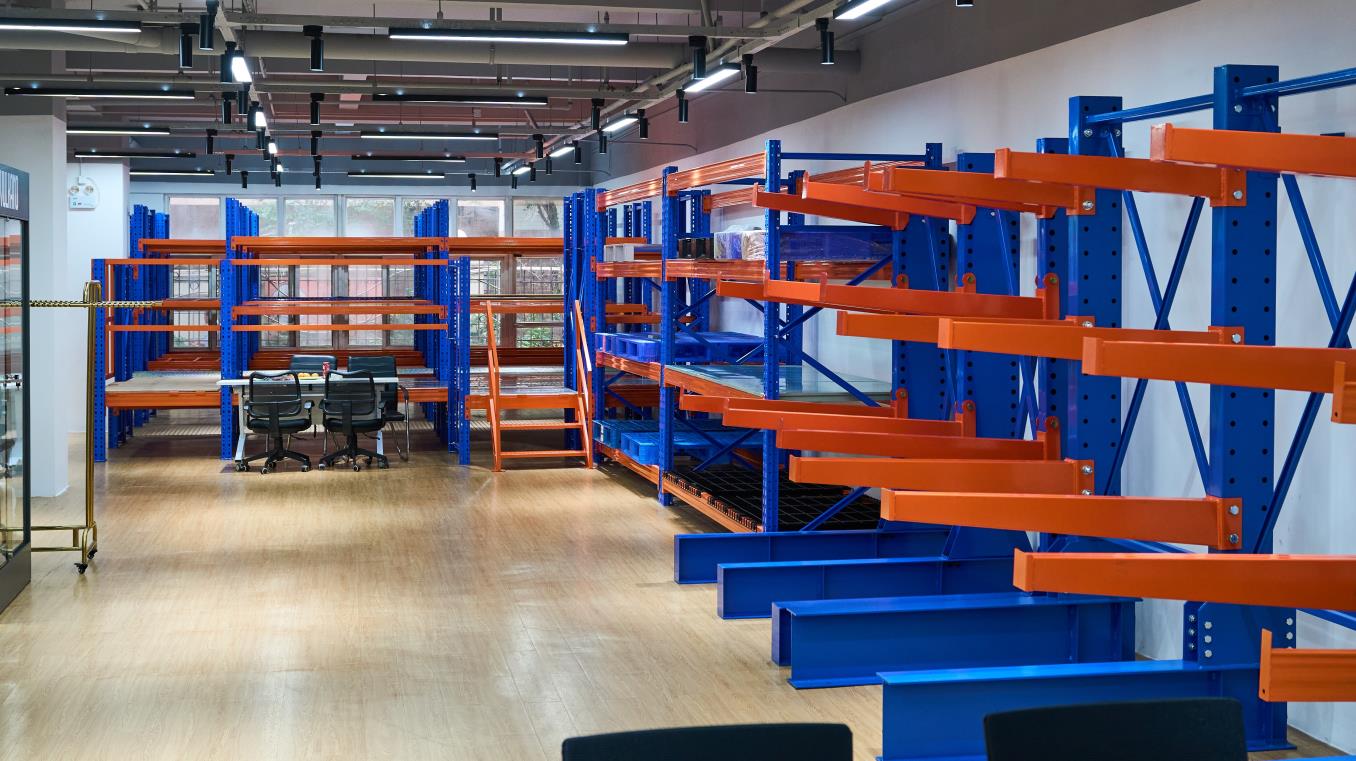
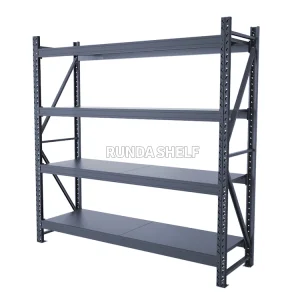
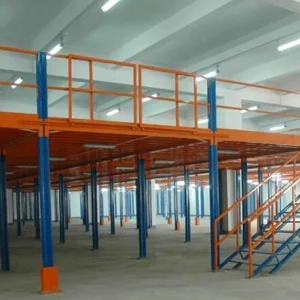
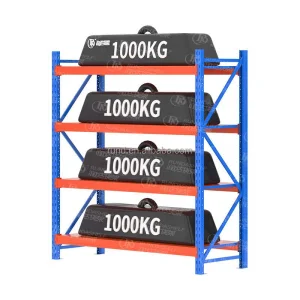
Our R&D capability focuses on High-Density Cantilever & Multi-Tier Mezzanine Engineering. We offer comprehensive custom options ranging from custom RAL color matching and specialized seismic-bracing to specialized rack protectors. Over the past year, we introduced 85 new product launches, developed by our team of 54 R&D engineers.
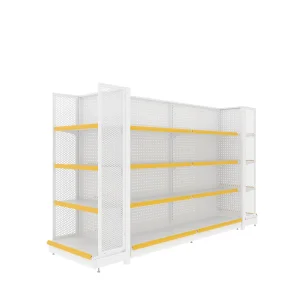
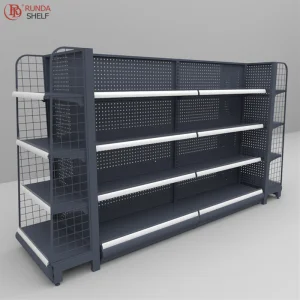
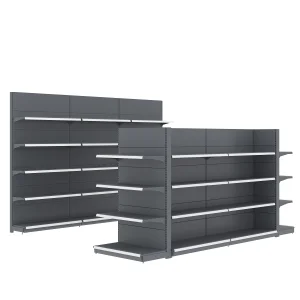
In the contemporary global retail and commercial landscape, CE Certified Professional Display Stands represent the critical convergence of ergonomic design, structural engineering, and brand merchandising strategy. As multinational retail chains and industrial distributors demand uncompromising quality, sourcing directly from top-tier Chinese manufacturing factories has become the cornerstone of international retail supply chain resilience.
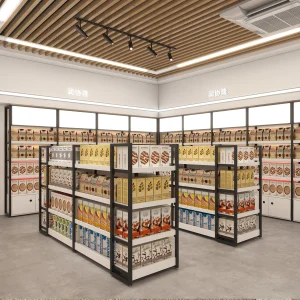
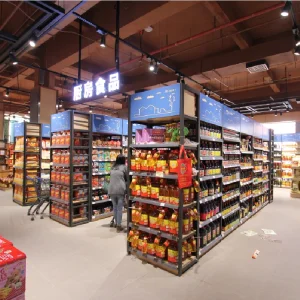
The global market for retail display stands and heavy-duty storage infrastructure is undergoing a massive transformation driven by omnichannel retail models. Physical stores are no longer mere warehouses of goods; they are immersive brand experience centers. Consequently, display stands must balance high load-bearing capacities with sleek, aesthetic finishes. Whether deployed in large-format supermarkets across Northern Europe, high-end pharmacies in North America, or commercial logistics hubs in Australia, modular display fixtures provide the flexibility required to adapt to rapidly changing consumer product lifecycles.
Different geographical regions impose distinct regulatory and environmental demands on display systems:
China's manufacturing ecosystem—exemplified by advanced industrial clusters in Ningbo—delivers unmatched supply chain efficiency. By integrating full-cycle in-line stress testing, laser coordinate measuring, and automated robotic welding, Tier-1 factories achieve economies of scale without compromising precision. The synergy of 1,850 localized component suppliers ensures uninterrupted production timelines, rapid prototyping, and cost-effective scaling for global turnkey projects.
The next decade will witness the accelerated integration of Smart Retail Technology into standard display structures. Key engineering milestones include:
Compliance with international standards (CE, ISO9001, AS/NZS) is non-negotiable. Professional manufacturing factories provide comprehensive engineering documentation, FEA (Finite Element Analysis) load-bearing simulation reports, and on-site installation supervision. This rigorous compliance framework mitigates liability for global buyers and ensures long-term operational safety.
 CrownRacking