The global retail and commercial storage ecosystem is undergoing a massive structural transformation. Driven by rapid omni-channel retail growth, hyper-urbanization, and the exponential expansion of e-commerce fulfillment hubs, modern supply chains demand unprecedented flexibility, structural durability, and spatial efficiency. Retailers can no longer rely on legacy static shelving units; instead, they require intelligent modular racking systems that integrate seamlessly with automated inventory tracking and high-density warehouse environments.
As enterprise procurement executives across North America, Northern Europe, and Australasia optimize their supply chain resilience, partnering with premier manufacturing hubs has become critical. The emphasis has shifted decisively toward factory-direct solutions capable of delivering customized load capacities, seismic-resistant engineering, and stringent international compliance standards (such as CE, ISO, and AS/NZS specifications).
China's manufacturing prowess in industrial storage infrastructure is anchored by mature industrial clusters, highly optimized supply chain ecosystems, and state-of-the-art automated production facilities. Leading manufacturing hubs—such as Ningbo—leverage advanced roll-forming machinery, robotic laser cutting systems, and electrostatic powder coating lines to produce high-tensile steel shelving with exceptional dimensional accuracy and surface corrosion resistance.
By streamlining raw material sourcing, vertical integration, and rigorous quality inspection protocols, top-tier factories achieve unmatched cost efficiencies without compromising structural integrity. This allows global enterprises to procure heavy-duty industrial storage racks and commercial display fixtures at highly competitive price points, backed by robust warranties and scalable production capacities.
Retail storage solutions span a diverse spectrum of operational environments, each demanding specialized design considerations:
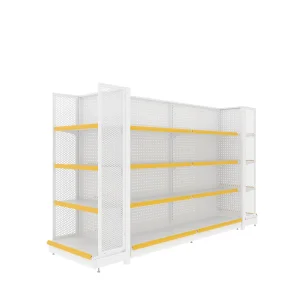
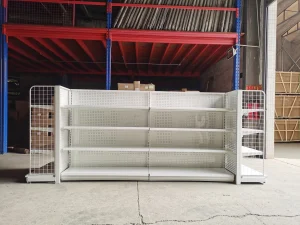
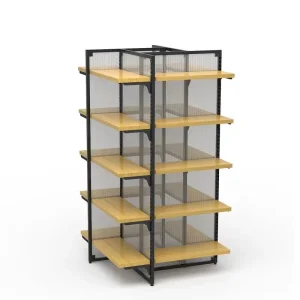
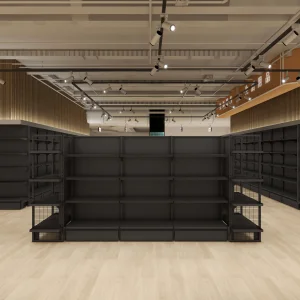
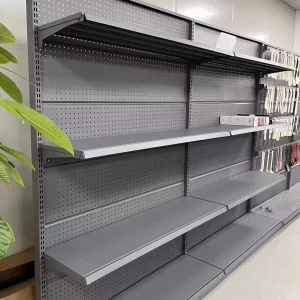
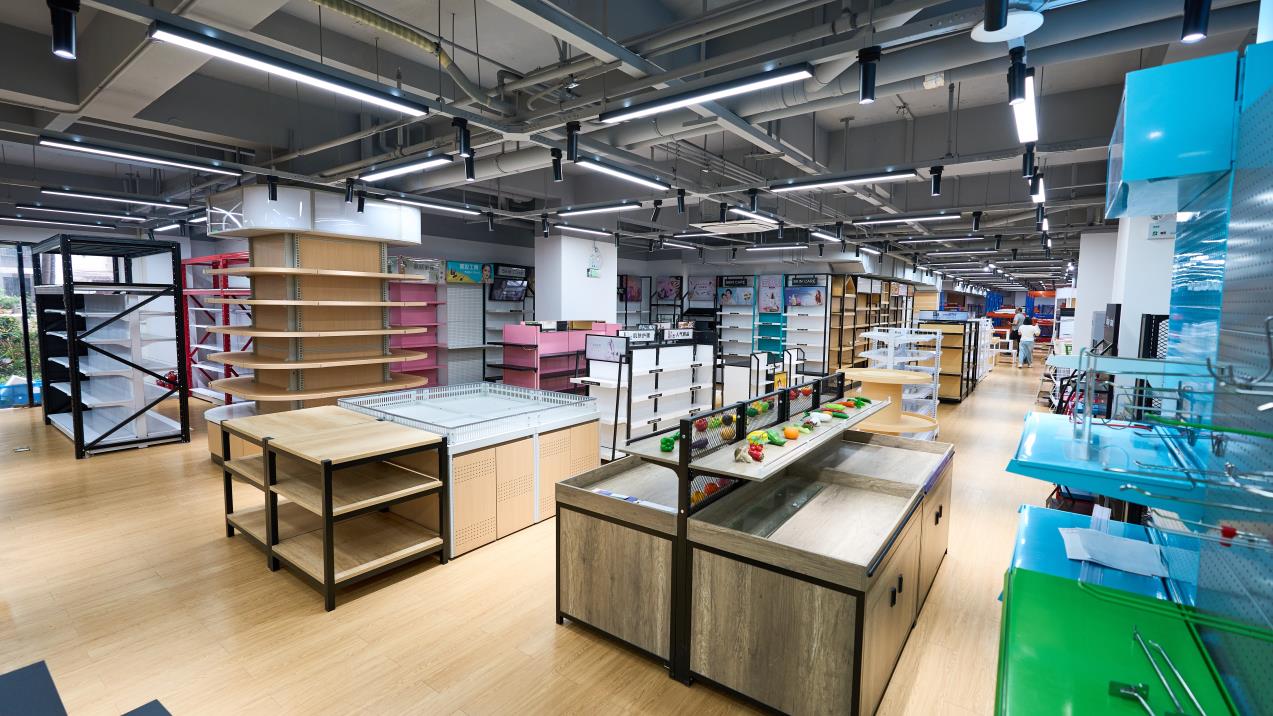
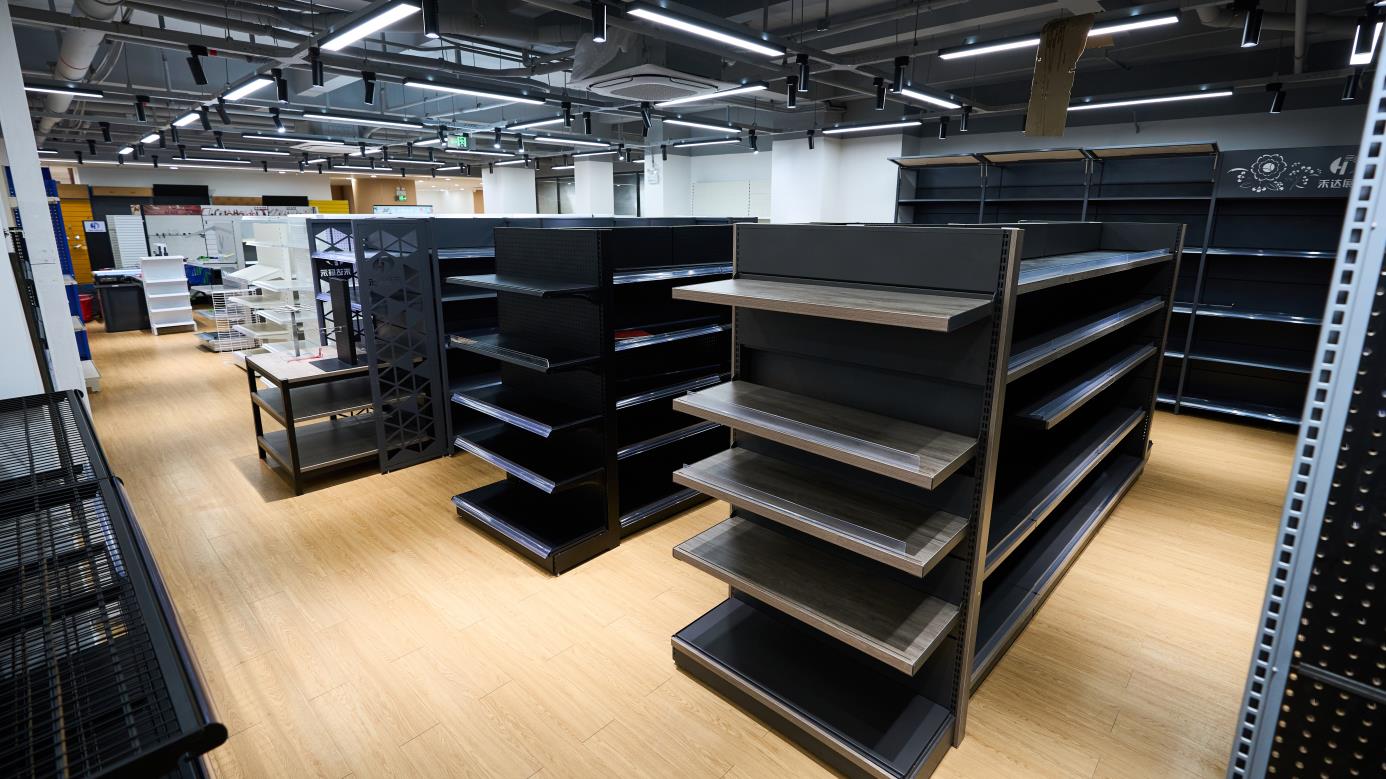
1. Hypermarkets and Supermarket Chains: Utilizing multi-tier gondola shelving, end-cap display units, and aesthetic promotional stands to maximize product visibility, facilitate consumer traffic flow, and drive impulse purchases.
2. Convenience Stores and Specialty Shops: Implementing compact light-duty metal combination shelves, grid wall panels, and modular checkout counters engineered for limited floor spaces and rapid inventory restocking.
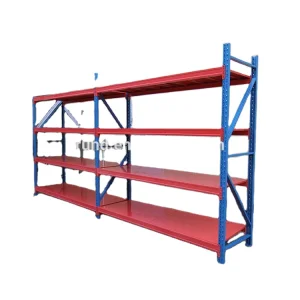
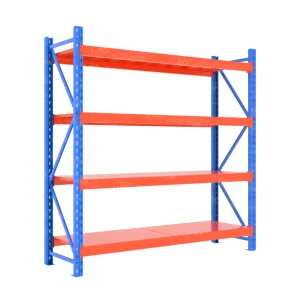
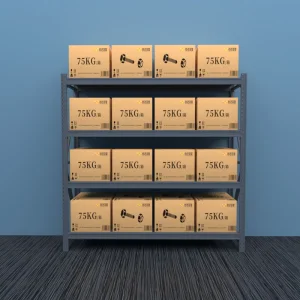
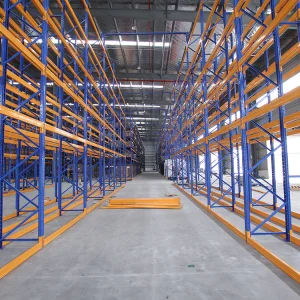
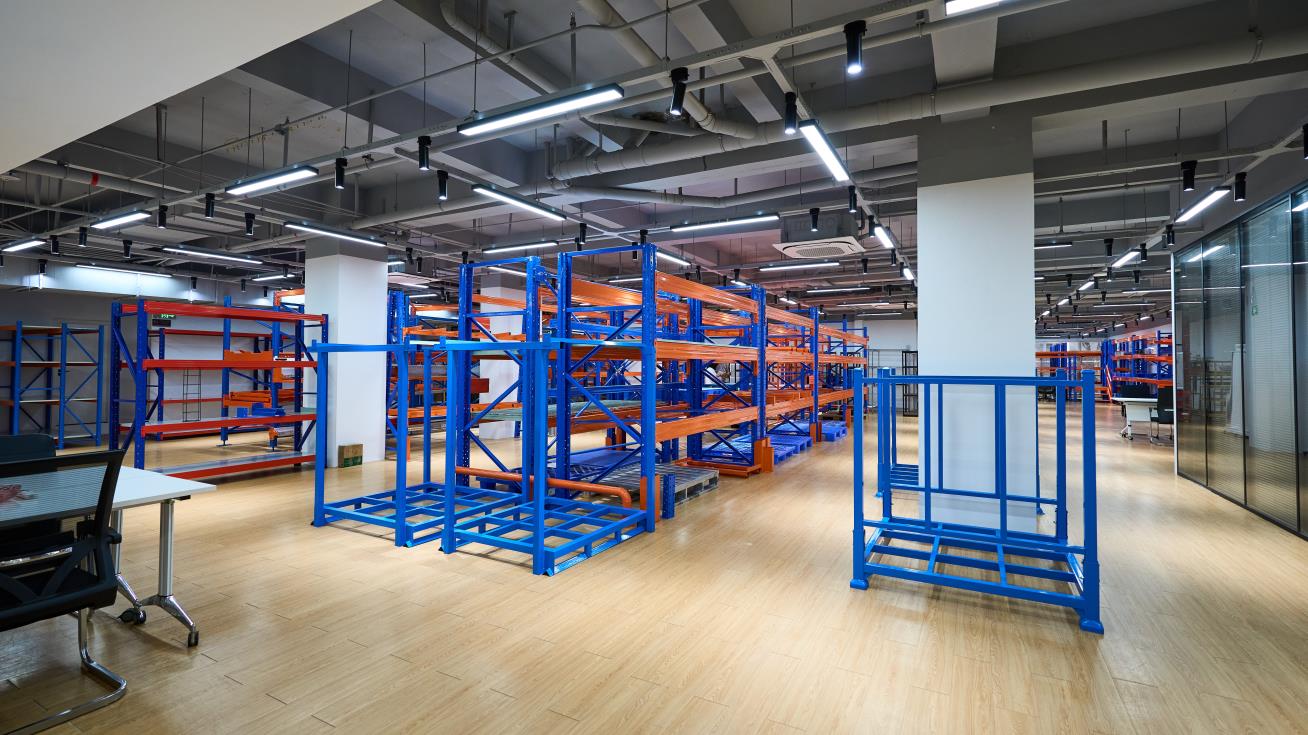
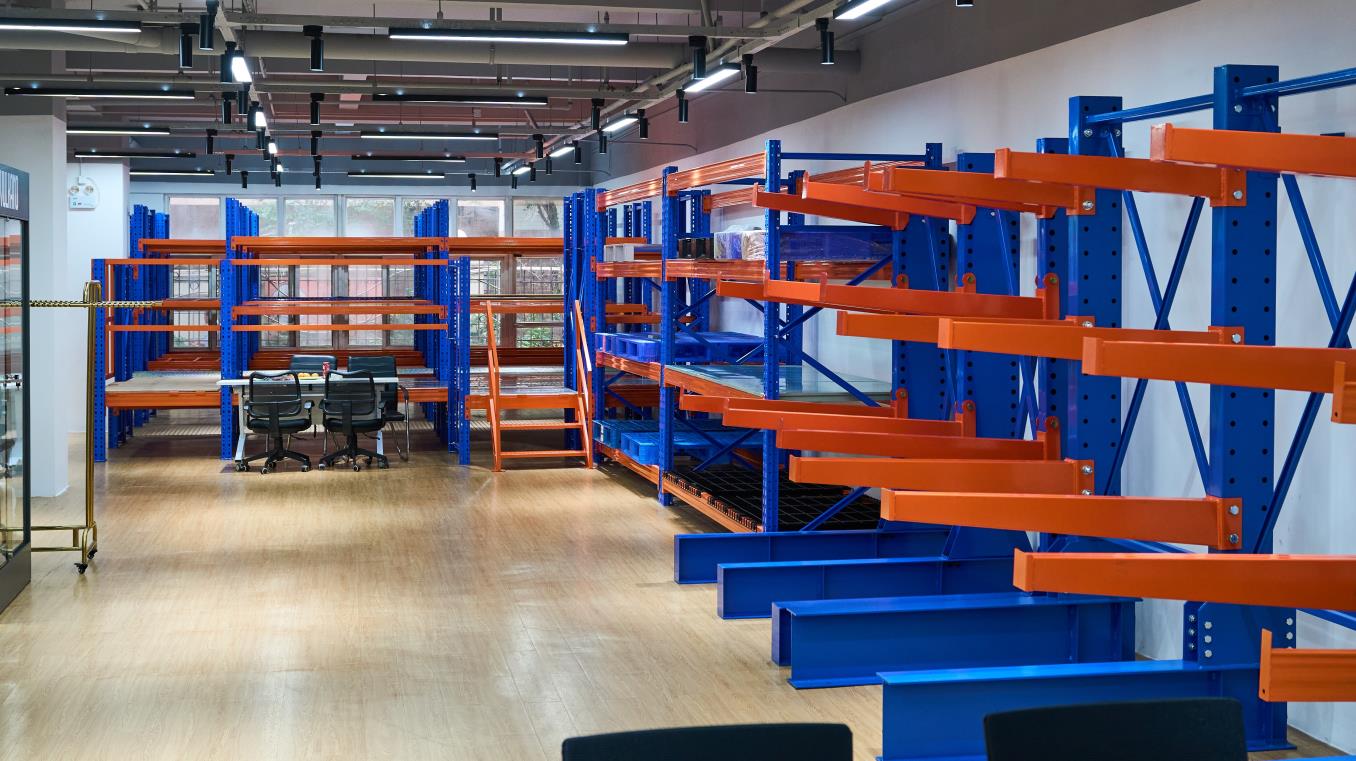
3. Heavy-Duty Warehouses & Logistics Parks: Deploying 5-layer metallic steel shelving, multi-level mezzanine racking, and cantilever systems designed to withstand dynamic load capacities ranging from 200kg to over 1000kg per tier.
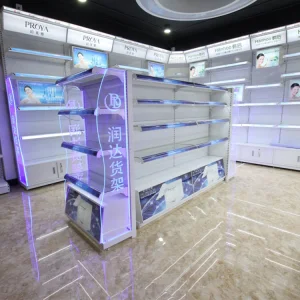
4. Pharmaceutical & Cleanroom Distribution: Requiring specialized antimicrobial powder-coated steel cabinets and square shelving units built for strict hygienic compliance and secure drug inventory control.
The next decade of retail storage engineering is defined by three major technological pillars:
• Intelligent Integration: The convergence of physical racking structures with IoT-enabled inventory sensors, Automated Storage and Retrieval Systems (AS/RS), and RFID tracking capabilities.
• Sustainable Manufacturing: Adoption of eco-friendly powder coating formulations, energy-efficient cold-roll forming processes, and recyclable steel alloys that align with global corporate ESG (Environmental, Social, and Governance) targets.
• Modular Customization: High demand for adaptable architectural configurations, bespoke RAL color matching, and seismic-braced frameworks tailored to regional engineering codes.
Ningbo CrownRacking Intelligent Warehouse Tech Co., Ltd. has been pioneering warehouse solutions since 2018. Operating out of a 46,500 m² modern production complex, we produce an annual export revenue of $42,000,000. Our operational success is backed by 5 years of international trade experience and 8 years of industry dedicated leadership.
We guarantee structural durability through rigorous Full-Cycle In-Line & Final Stress Load Inspection, employing Laser Coordinate Measuring & Coating Thickness Verification managed by 62 QC staff members. With a Factory Direct Exporter with Global Turnkey Project Services trade background, our primary markets cover Australia, Northern Europe, and North America. We are supported by 1,850 supply chain partners, serving major client types including pharmaceutical distribution networks, retail logistics parks, and heavy machinery warehouses.
Our R&D capability focuses on High-Density Cantilever & Multi-Tier Mezzanine Engineering. We offer comprehensive custom options ranging from custom RAL color matching and specialized seismic-bracing to specialized rack protectors. Over the past year, we introduced 85 new product launches, developed by our team of 54 R&D engineers.
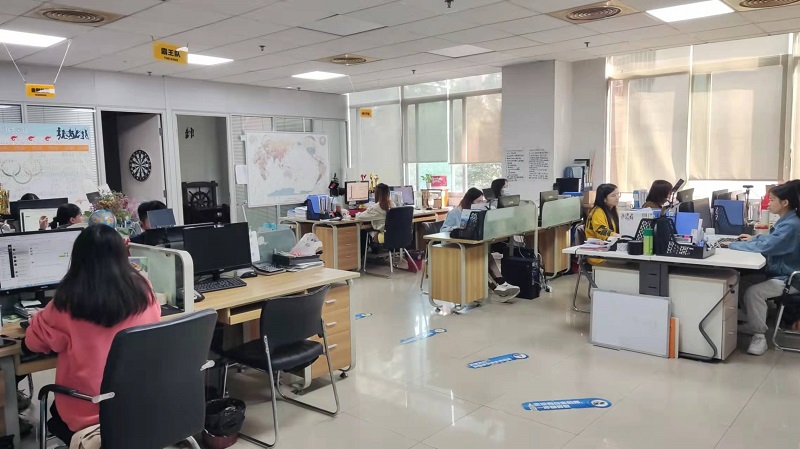 Production Facility
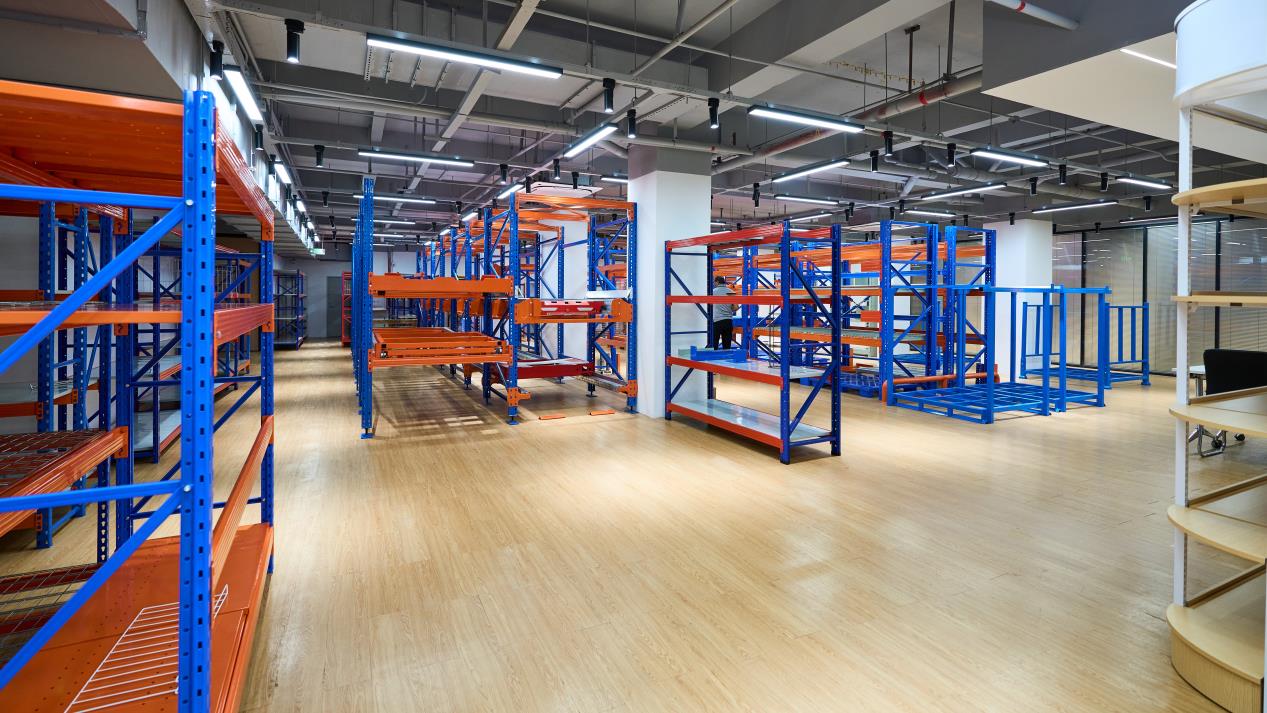 Automated Line
 Assembly Floor
 Quality Inspection
 Finished Goods
 Global Shipping
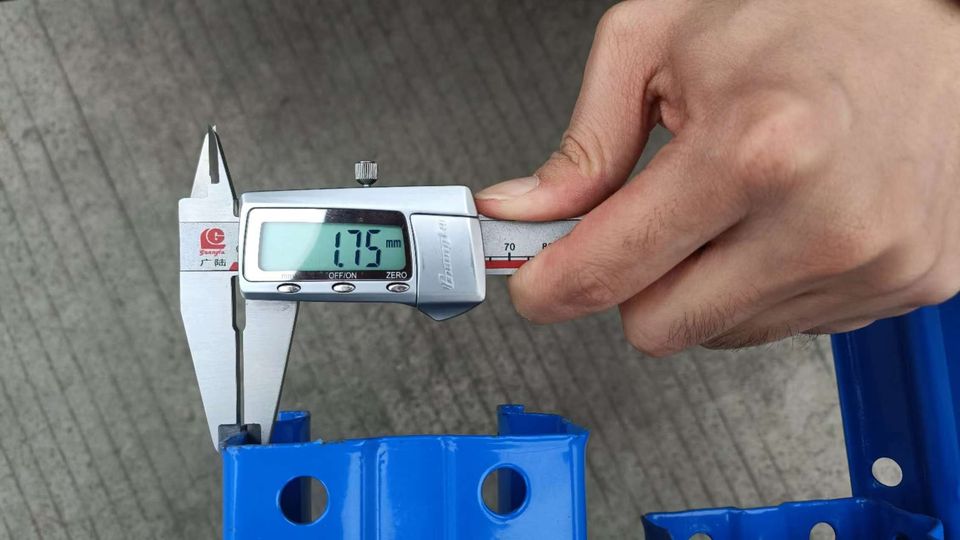 Caliper
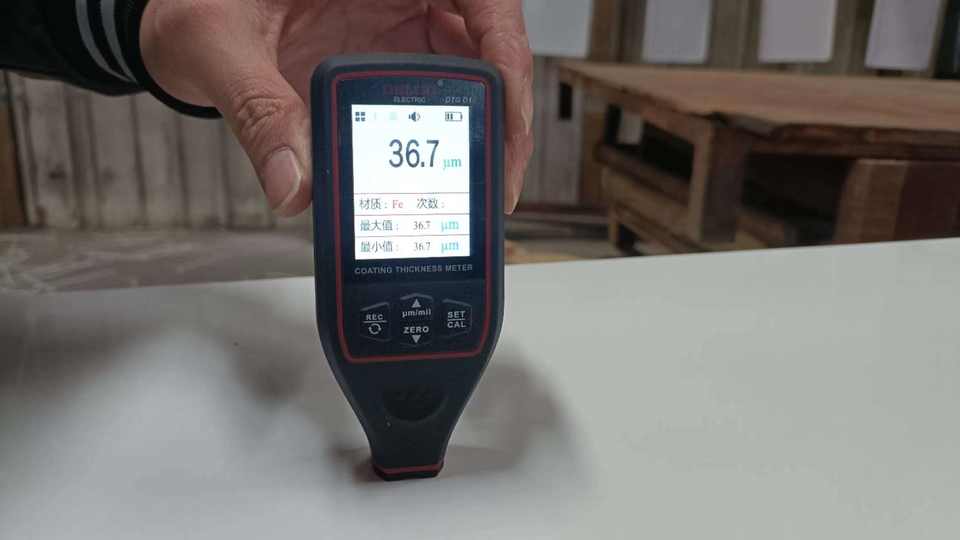 Coating thickness tester
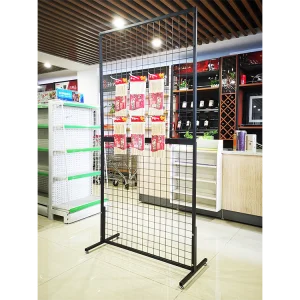
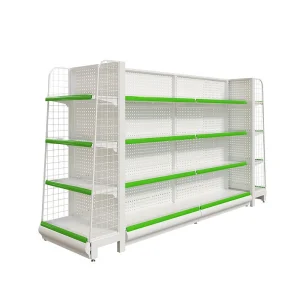
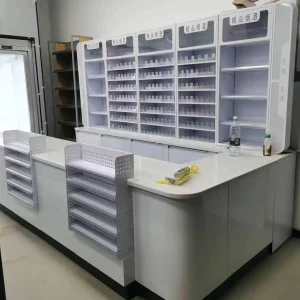
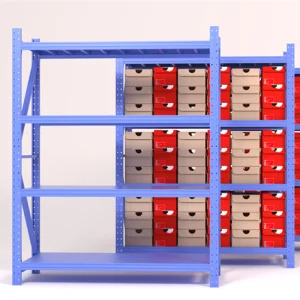
Our heavy-duty industrial storage racks and multi-layer metallic steel shelves are engineered to support dynamic loads ranging from 200kg up to 1000kg+ per tier. Custom load-bearing specifications and seismic-braced frameworks are also available upon request.
Yes. With a dedicated team of 54 R&D engineers and 85 annual product launches, we offer comprehensive custom solutions including bespoke RAL color matching, specialized dimensions, branded signage integration, and tailored grocery shelving layouts.
Our manufacturing process is backed by 62 dedicated QC staff members utilizing laser coordinate measuring instruments, coating thickness verification testers, and full-cycle in-line and final stress load inspections to guarantee superior structural longevity.
We primarily export to commercial logistics parks, retail distribution networks, and pharmaceutical warehouses across Australia, Northern Europe, and North America, offering comprehensive global turnkey project coordination.
 CrownRacking