Explore our high-performance display racks and modular shelving systems manufactured for commercial enterprise deployment.
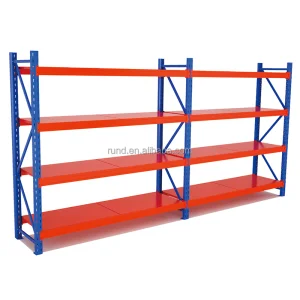
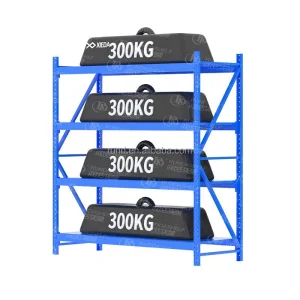
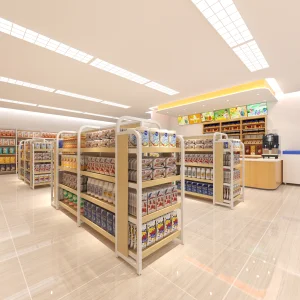
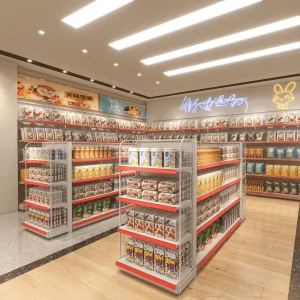
The global commercial display and industrial exhibition rack ecosystem is experiencing a structural paradigm shift driven by modern omni-channel retail architecture, rapid warehouse automation, and dynamic trade show presentation requirements. Modern commercial spaces no longer view exhibition racks as static storage hardware; instead, they are engineered architectural components designed to optimize floor space utilization, elevate brand visibility, and withstand intensive structural loads in high-traffic environments.
As enterprise procurement shifts toward modularity, structural durability, and rapid assembly, top-tier exhibition rack manufacturers must integrate advanced metallurgy with intelligent industrial design. The demand across Northern Europe, North America, and Australia emphasizes high load-bearing capacity, customizable grid configurations, and zero-defect surface finishes capable of enduring continuous dynamic forces.
Information Gain Key Metric: Global commercial exhibition racking and high-density store fixtures are projected to reach a CAGR of 6.4% through 2030, driven predominantly by high-density pharmacy automation, heavy-duty grocery gondolas, and modular trade show display architectures.
To qualify as a leading exhibition racks manufacturer, structural integrity must be validated through rigorous mechanical engineering protocols. Premium storage and display systems utilize high-tensile cold-rolled steel alloys (such as Q235B and Q355B grades), offering superior yield strength (up to 355 MPa) and exceptional resistance to flexural deformation under asymmetrical static loads.
Every beam profile, cantilever arm, and perforated backpanel undergoes simulated stress vector analysis to prevent fatigue failure under maximum load tolerances.
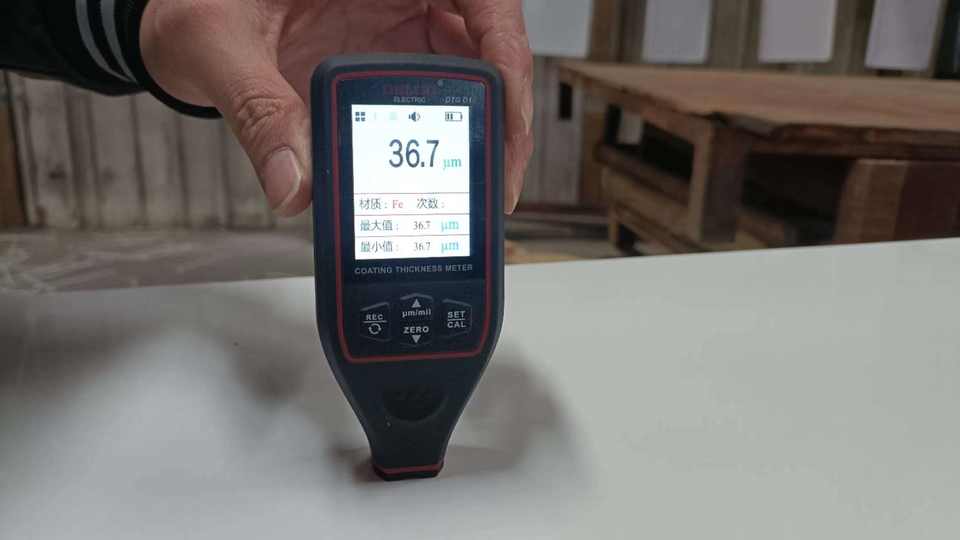
Utilizing high-voltage automated powder coating lines, rack surfaces achieve 60-90 micron film thickness, providing anti-corrosion, scratch-resistant protection.
Custom rack structures are engineered with specialized upright column pitch patterns and heavy-duty base plates compliant with international seismic safety codes.
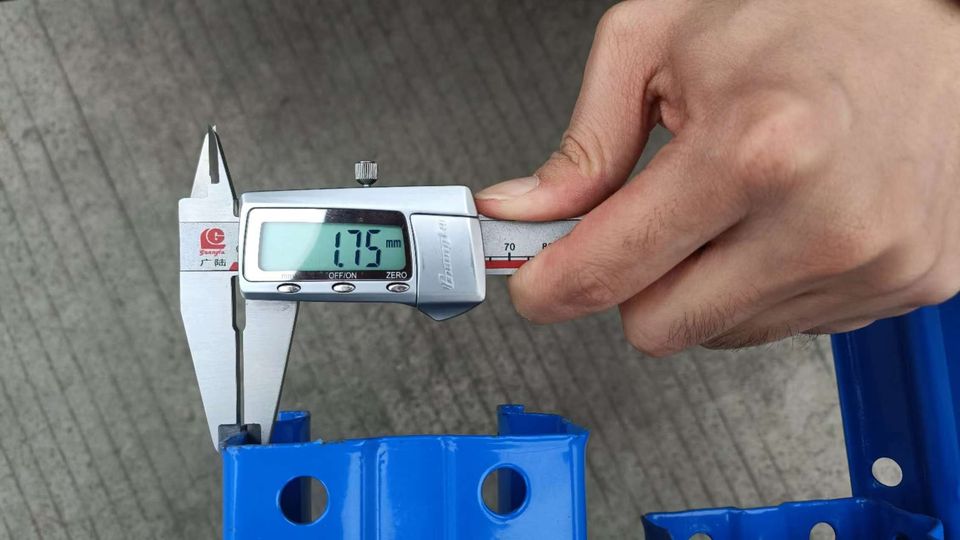
The convergence of modern automation and industrial exhibition rack fabrication has enabled unprecedented production efficiency. Advanced factories deploy robotic fiber-laser cutting stations, multi-axis automated CNC bending machines, and continuous roll-forming production lines. This automated infrastructure ensures dimensional pitch tolerances within ±0.1mm—an essential benchmark for seamless boltless snap-in assembly and interchangeable component modularity.
Furthermore, eco-conscious manufacturing practices have become central to Tier-1 factory operations. By implementing closed-loop water treatment systems and non-toxic zinc-phosphate pre-treatment washes, high-capacity racking facilities reduce environmental impact while achieving superior paint adhesion and impact resistance standards required by global buyers.
Industrial display and exhibition racks must adapt to diverse commercial environments, each demanding distinct structural characteristics, ergonomic considerations, and visual styling:
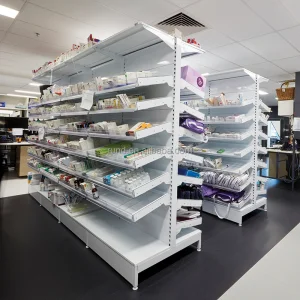
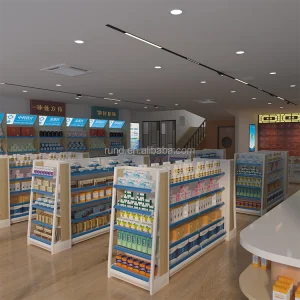
Demands hygienic, smooth powder-coated modular drawer racks with high-density divider trays. Designed for rapid inventory picking, hospital-grade sanitation, and security locking mechanisms.
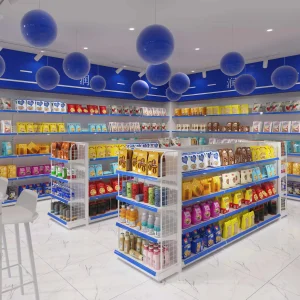
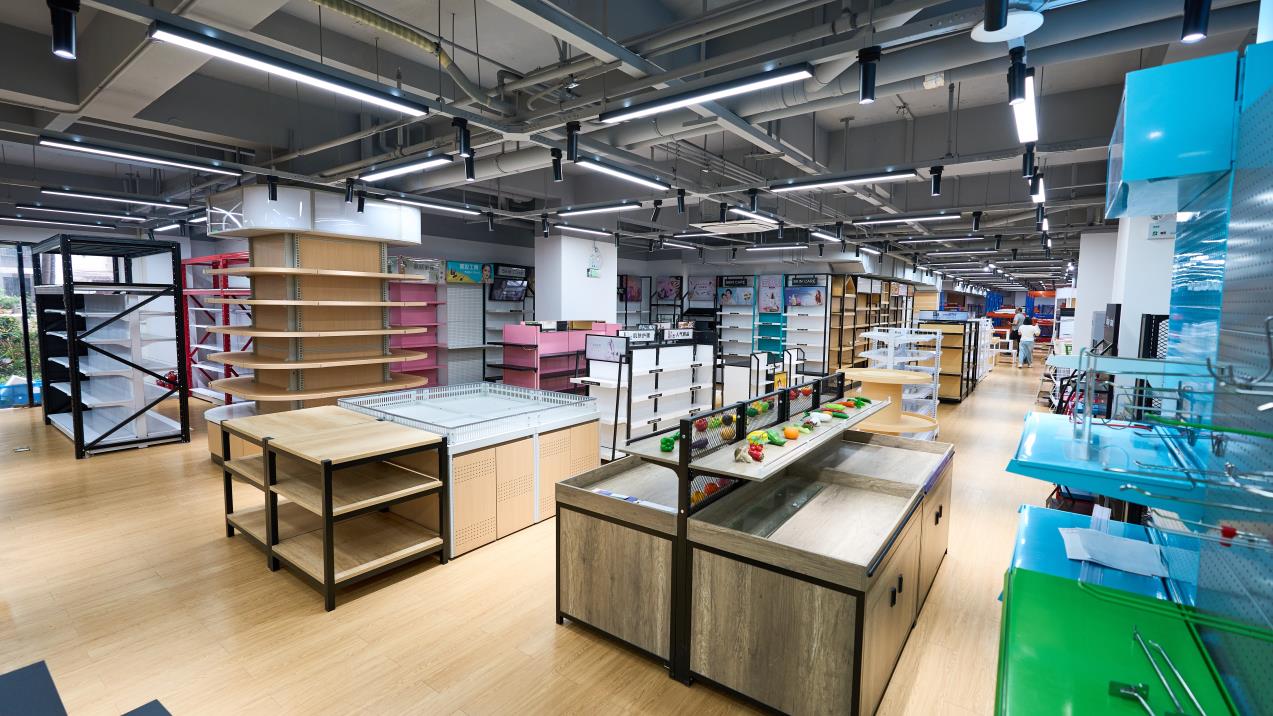
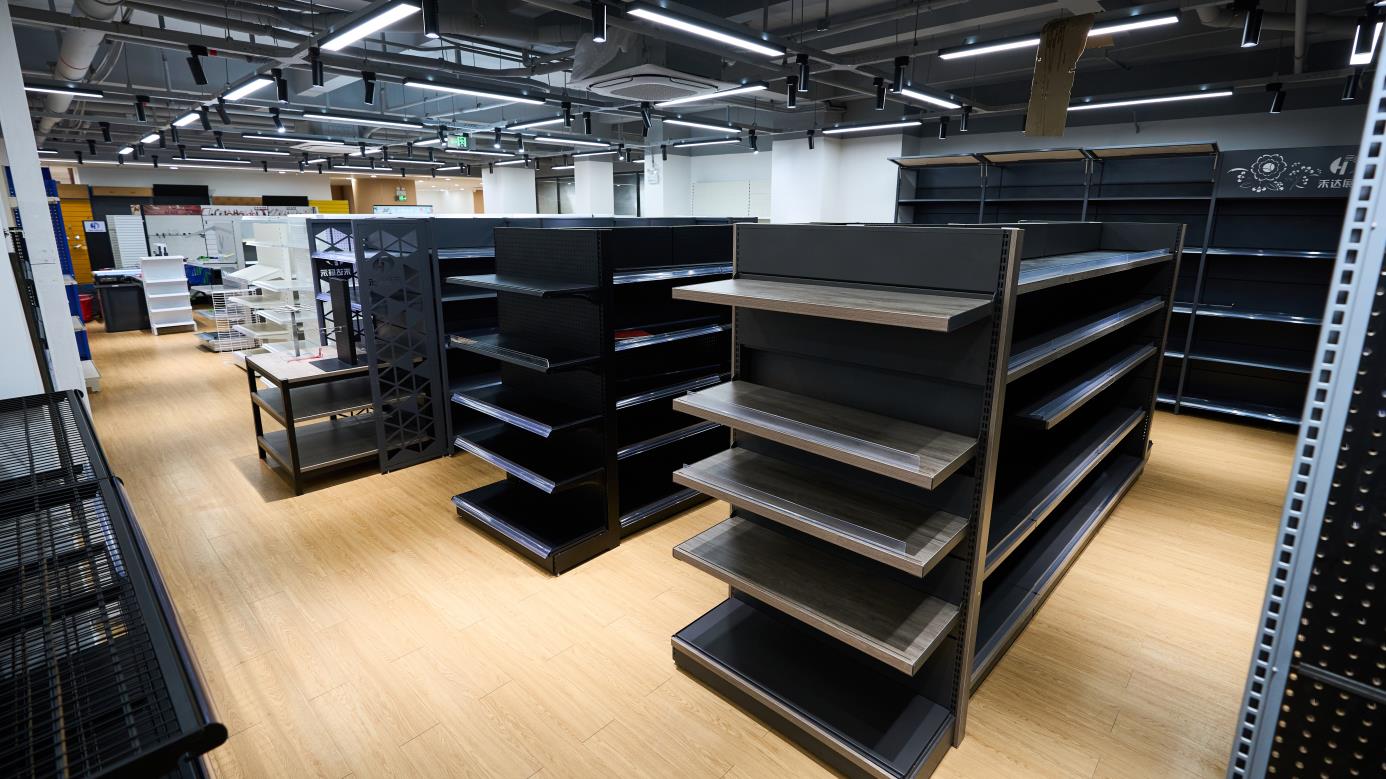
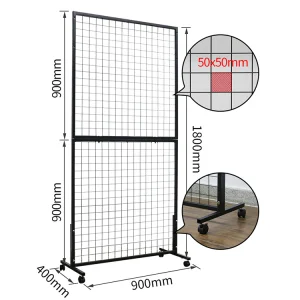
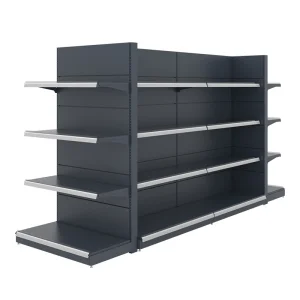
Employs double-sided middle-island gondolas and perforated pegboard backpanels. Capable of supporting heavy merchandise weight while maintaining customizable shelf spacing and integration with automated pricing rails.
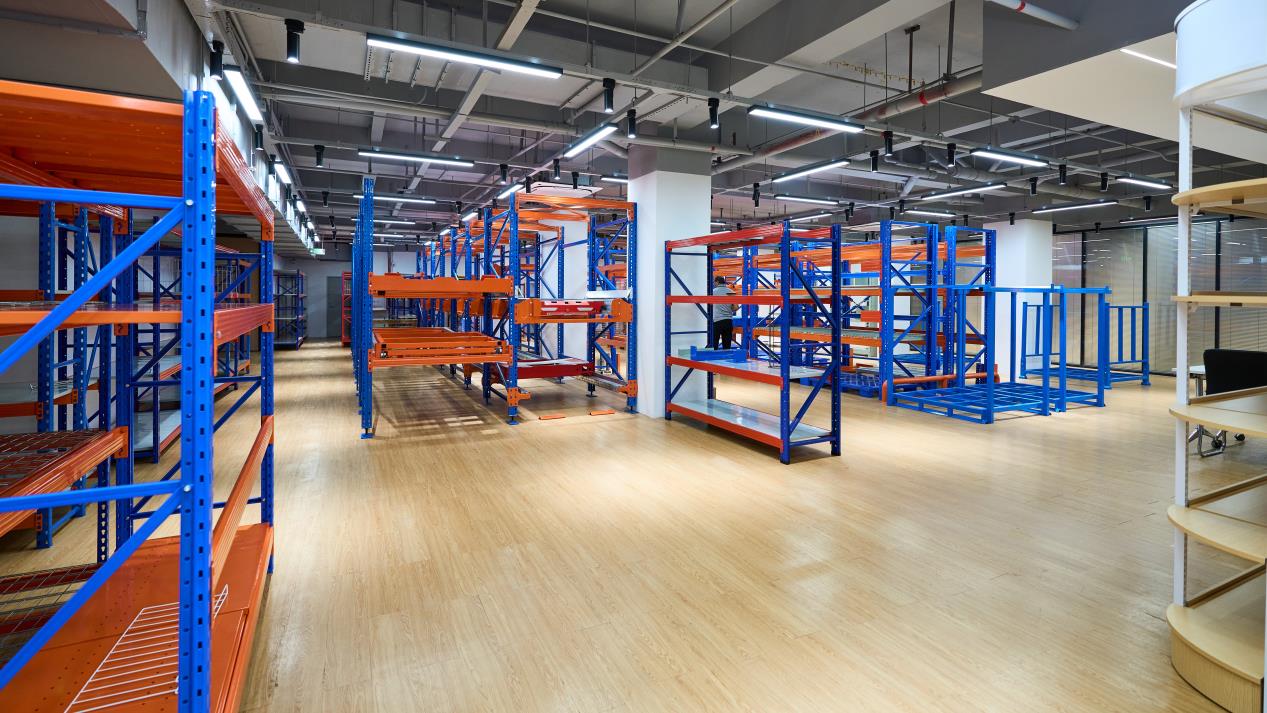
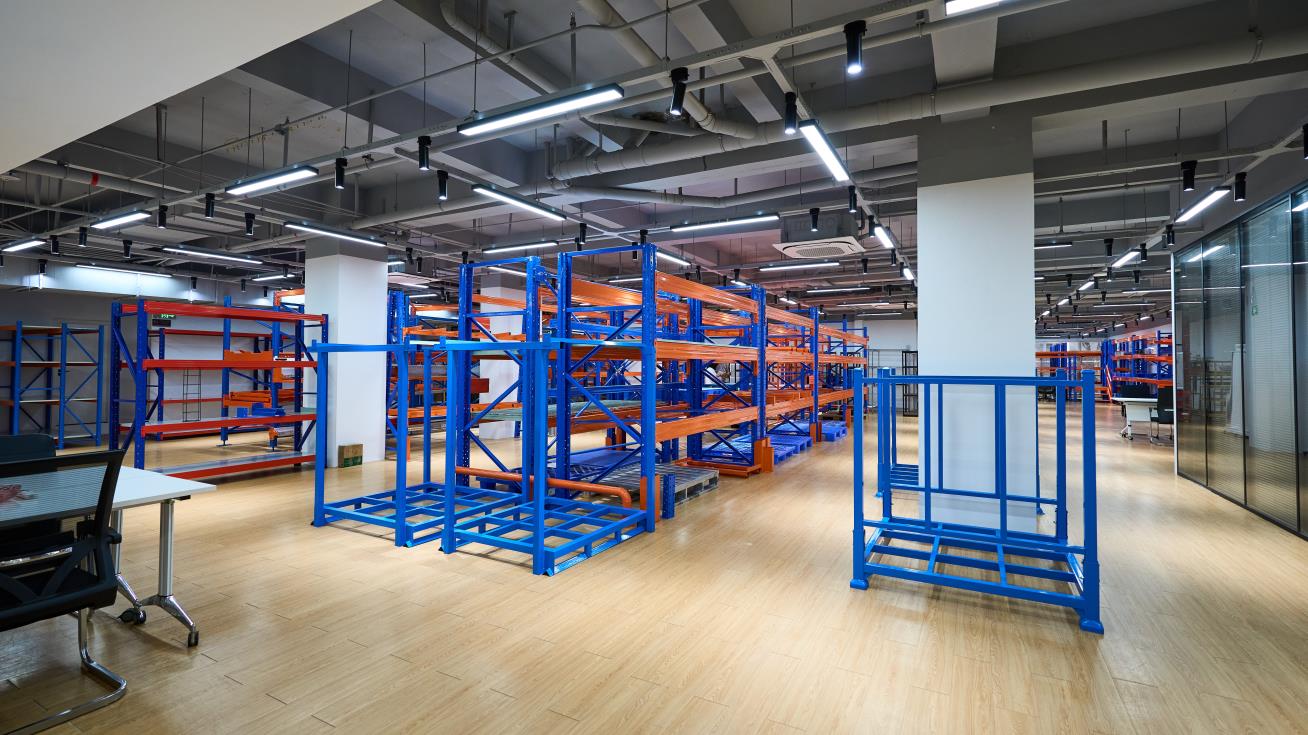
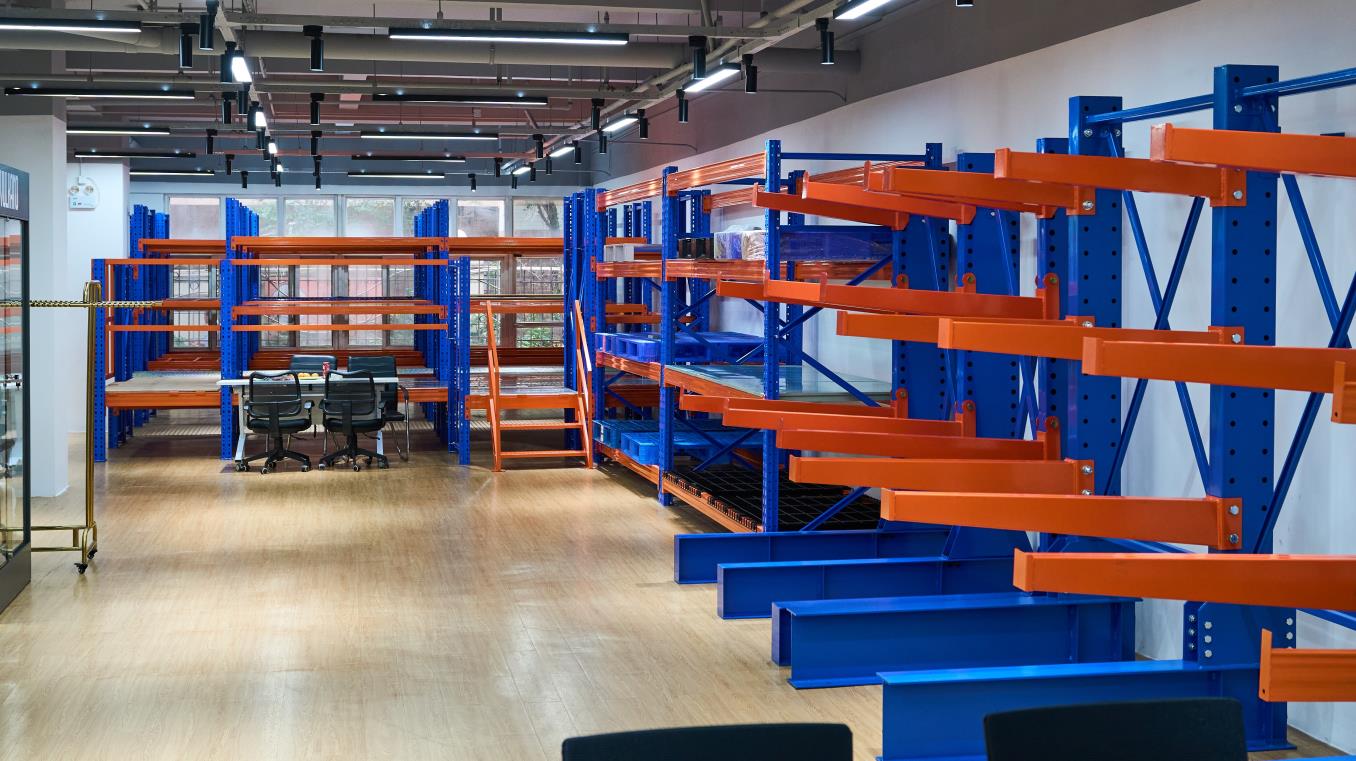
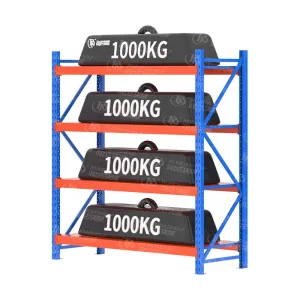
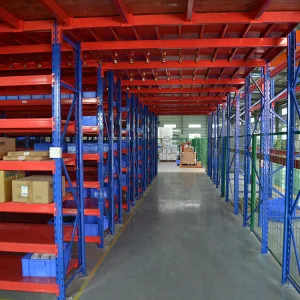
Utilizes cantilever racks and high-density crossbeam systems capable of supporting loads up to 1,000kg per level. Built for heavy machinery parts, raw material storage, and forklift accessibility.
The display rack manufacturing sector is rapidly advancing toward intelligent, dynamic, and ultra-modular operational frameworks. Industry leaders are investing heavily in next-generation structural R&D:
Integration of embedded weight sensors and RFID tracking grids directly within shelf beams for real-time inventory management.
Transition toward 100% recycled structural steel alloys and zero-VOC waterborne thermosetting powder coatings.
Development of zero-tool, high-load locking connectors that reduce exhibit booth and store setup times by 65%.
Algorithm-assisted modular shelf design software that calculates optimal beam placement based on historical retail sales velocity.
Demonstrating industry-leading expertise, technical transparency, and rigorous quality control standards.
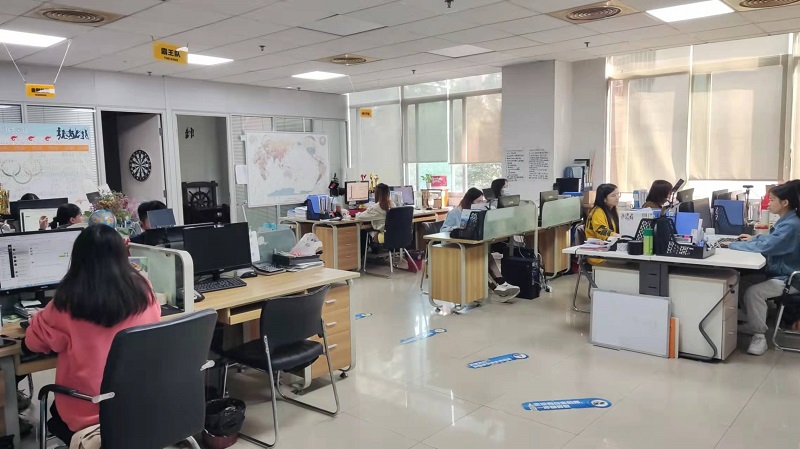
Ningbo CrownRacking Intelligent Warehouse Tech Co., Ltd. has been pioneering warehouse solutions since 2018. Operating out of a 46,500 m² modern production complex, we produce an annual export revenue of $42,000,000. Our operational success is backed by 5 years of international trade experience and 8 years of industry dedicated leadership.
We guarantee structural durability through rigorous Full-Cycle In-Line & Final Stress Load Inspection, employing Laser Coordinate Measuring & Coating Thickness Verification managed by 62 QC staff members. With a Factory Direct Exporter with Global Turnkey Project Services trade background, our primary markets cover Australia, Northern Europe, and North America. We are supported by 1,850 supply chain partners, serving major client types including pharmaceutical distribution networks, retail logistics parks, and heavy machinery warehouses.
Our R&D capability focuses on High-Density Cantilever & Multi-Tier Mezzanine Engineering. We offer comprehensive custom options ranging from custom RAL color matching and specialized seismic-bracing to specialized rack protectors. Over the past year, we introduced 85 new product launches, developed by our team of 54 R&D engineers.
Addressing engineering specifications, customization options, and global supply chain logistics.
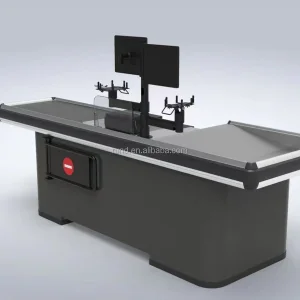
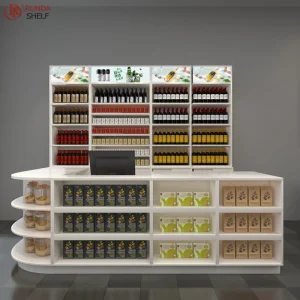
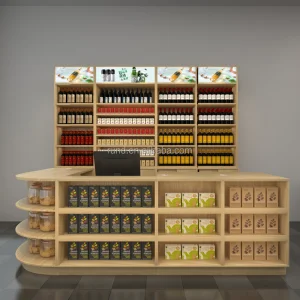
High-density industrial shelving, cantilever storage units, and specialized cashier checkout counters.
 CrownRacking