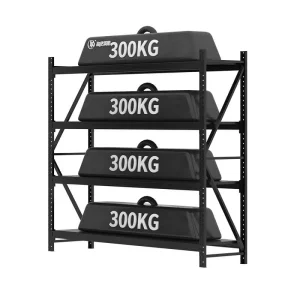
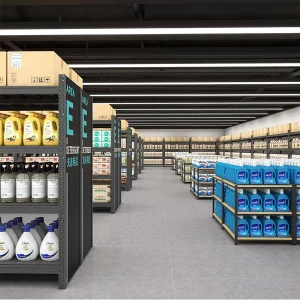
Optimized for small-to-medium inventory management, retail backrooms, and industrial component sorting in Mbarara.
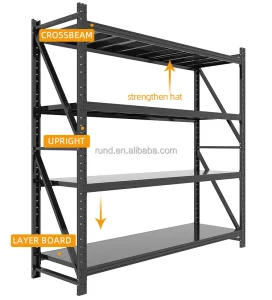
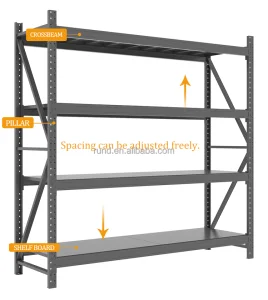
Mbarara, famously known as the commercial hub of southwestern Uganda, is witnessing an unprecedented surge in agro-processing, retail distribution, pharmaceutical warehousing, and light manufacturing. As regional supply chains expand to connect Kampala with the Democratic Republic of Congo (DRC) and Rwanda, the demand for efficient space optimization has skyrocketed.
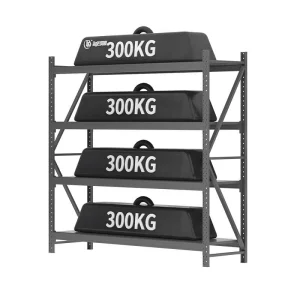
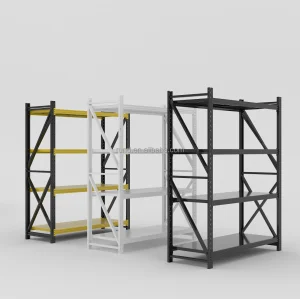
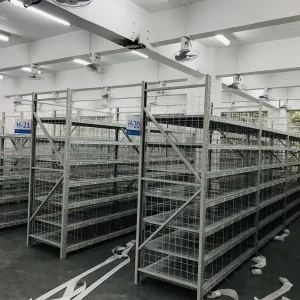
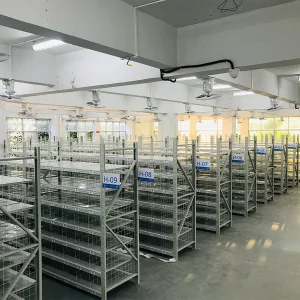
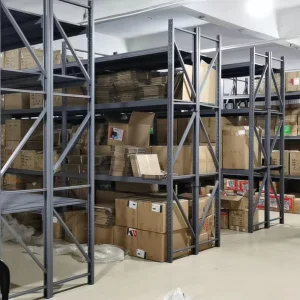
Our Light Warehouse Shelves (<300KG) are specifically engineered to withstand local climatic conditions while maximizing vertical storage space in urban storefronts, agricultural produce collection centers, and cold-chain distribution hubs. By utilizing high-grade Q235 steel with advanced powder coating, these racks resist humidity and wear, ensuring long-term operational viability for Mbarara enterprises.
The future of logistics in East Africa relies on smart inventory integration and modular adaptability. Our structural engineering roadmap incorporates boltless assembly systems, eco-friendly surface treatments, and seismic-resistant tier designs. This allows Mbarara business owners to effortlessly scale their warehouse capacity from small modular units to multi-tier shelving setups without structural downtime.
Backed by decades of manufacturing expertise, our production complex spans 46,500 m², empowering us to maintain a robust supply chain network supported by 1,850 supply chain partners. We bridge the gap between world-class Chinese manufacturing efficiency and the localized infrastructure requirements of emerging commercial centers like Mbarara.
Every shelving unit undergoes strict quality assurance protocols, including laser coordinate measuring and coating thickness verification by our 62 dedicated QC staff members, ensuring international standards (GS certified) are consistently delivered to our global clientele across North America, Northern Europe, Australia, and East Africa.
Pioneering intelligent warehouse solutions since 2018 with global turnkey project execution capabilities.
Ningbo CrownRacking Intelligent Warehouse Tech Co., Ltd. has been pioneering warehouse solutions since 2018. Operating out of a 46,500 m² modern production complex, we produce an annual export revenue of $42,000,000. Our operational success is backed by 5 years of international trade experience and 8 years of industry dedicated leadership.
We guarantee structural durability through rigorous Full-Cycle In-Line & Final Stress Load Inspection, employing Laser Coordinate Measuring & Coating Thickness Verification managed by 62 QC staff members. With a Factory Direct Exporter with Global Turnkey Project Services trade background, our primary markets cover Australia, Northern Europe, and North America. We are supported by 1,850 supply chain partners, serving major client types including pharmaceutical distribution networks, retail logistics parks, and heavy machinery warehouses.
Our R&D capability focuses on High-Density Cantilever & Multi-Tier Mezzanine Engineering. We offer comprehensive custom options ranging from custom RAL color matching and specialized seismic-bracing to specialized rack protectors. Over the past year, we introduced 85 new product launches, developed by our team of 54 R&D engineers.
Expert answers regarding our light warehouse shelving solutions for Mbarara clients.
Comprehensive heavy-duty, medium-duty, and specialized industrial storage options engineered for global performance.
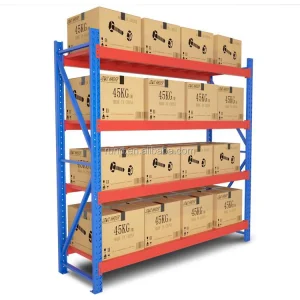
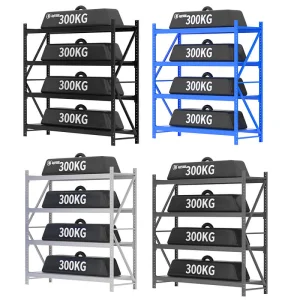
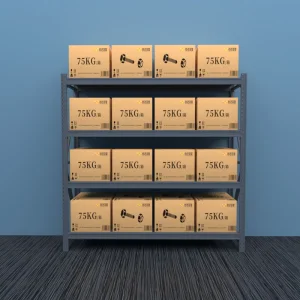
 CrownRacking