Explore our high-demand OEM/ODM industrial and commercial racking systems engineered for maximum durability and space efficiency.
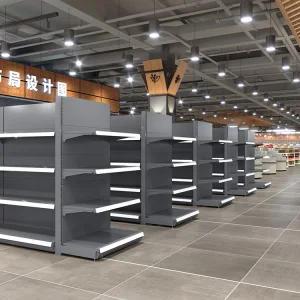
A comprehensive analysis of market evolution, supply chain modernization, and rising B2B sourcing standards.
Global enterprises and commercial giants are rapidly transitioning away from generic, off-the-shelf storage modules. Modern procurement strategies heavily prioritize modular, custom OEM utility shelving engineered to withstand high-capacity loads while optimizing vertical warehouse footprints. Supply chain executives across North America, Northern Europe, and Australia mandate rigorous structural compliance and corrosion-resistant finishes.
Driven by the continuous expansion of e-commerce fulfillment centers, automated retail logistics parks, and specialized pharmaceutical supply chains, the global demand for heavy-duty industrial shelving has experienced exponential growth. B2B buyers now evaluate suppliers based on rapid custom prototyping, precise load-bearing capabilities, and seamless integration with automated storage retrieval systems (ASRS).
Sourcing directly from advanced manufacturing hubs provides global businesses with unmatched cost efficiency without compromising on structural integrity. Direct factory partnerships enable bespoke design adaptations, including proprietary RAL color matching, customized seismic-bracing, and modular multi-tier mezzanine scaling tailored to complex architectural environments.
How advanced automation, precision metrology, and strict quality control redefine global industrial standards.
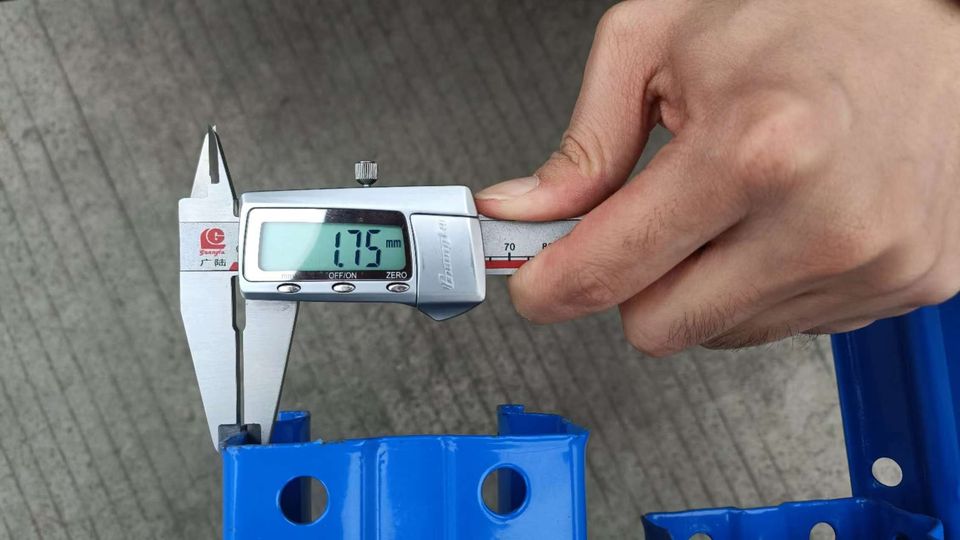
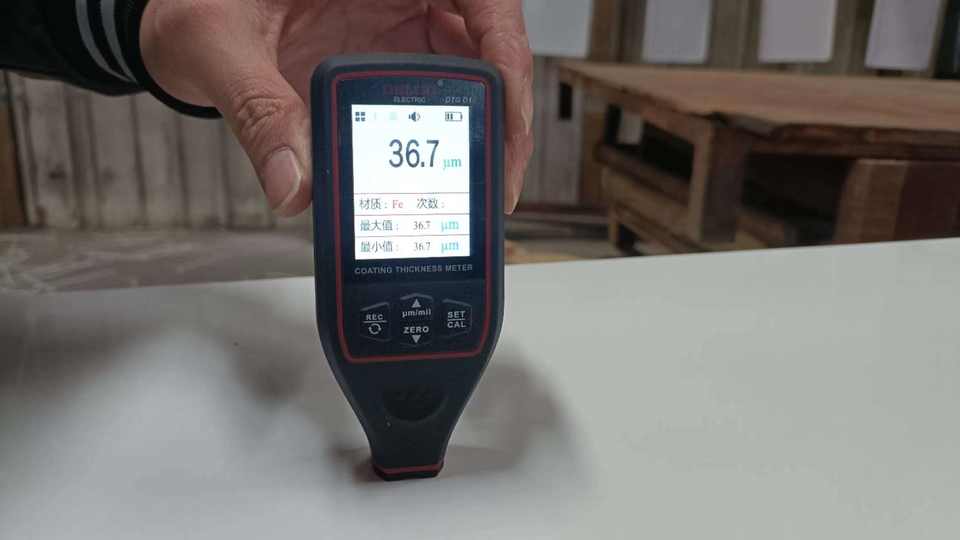
The evolution of modern manufacturing in top-tier industrial facilities—exemplified by Ningbo CrownRacking Intelligent Warehouse Tech Co., Ltd.—leverages Industry 4.0 automation. By integrating Laser Coordinate Measuring & Coating Thickness Verification, every batch of utility shelving undergoes uncompromising stress testing.
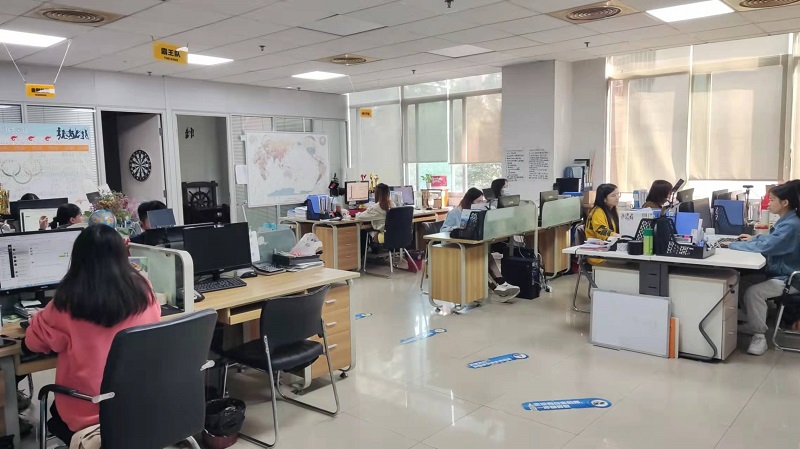
Our operational ecosystem is anchored by stringent Full-Cycle In-Line & Final Stress Load Inspection protocols. From raw cold-rolled steel selection to automated robotic welding and electrostatic powder coating, our 54 R&D engineers and 62 quality control inspectors ensure that every rack meets international seismic and load safety standards. This unmatched manufacturing rigor guarantees superior durability for high-density industrial deployments.
Decade-long industry leadership delivering turnkey warehouse racking solutions worldwide.
Ningbo CrownRacking Intelligent Warehouse Tech Co., Ltd. has been pioneering warehouse solutions since 2018. Operating out of a 46,500 m² modern production complex, we produce an annual export revenue of $42,000,000. Our operational success is backed by 5 years of international trade experience and 8 years of industry dedicated leadership.
We guarantee structural durability through rigorous Full-Cycle In-Line & Final Stress Load Inspection, employing Laser Coordinate Measuring & Coating Thickness Verification managed by 62 QC staff members. With a Factory Direct Exporter with Global Turnkey Project Services trade background, our primary markets cover Australia, Northern Europe, and North America. We are supported by 1,850 supply chain partners, serving major client types including pharmaceutical distribution networks, retail logistics parks, and heavy machinery warehouses.
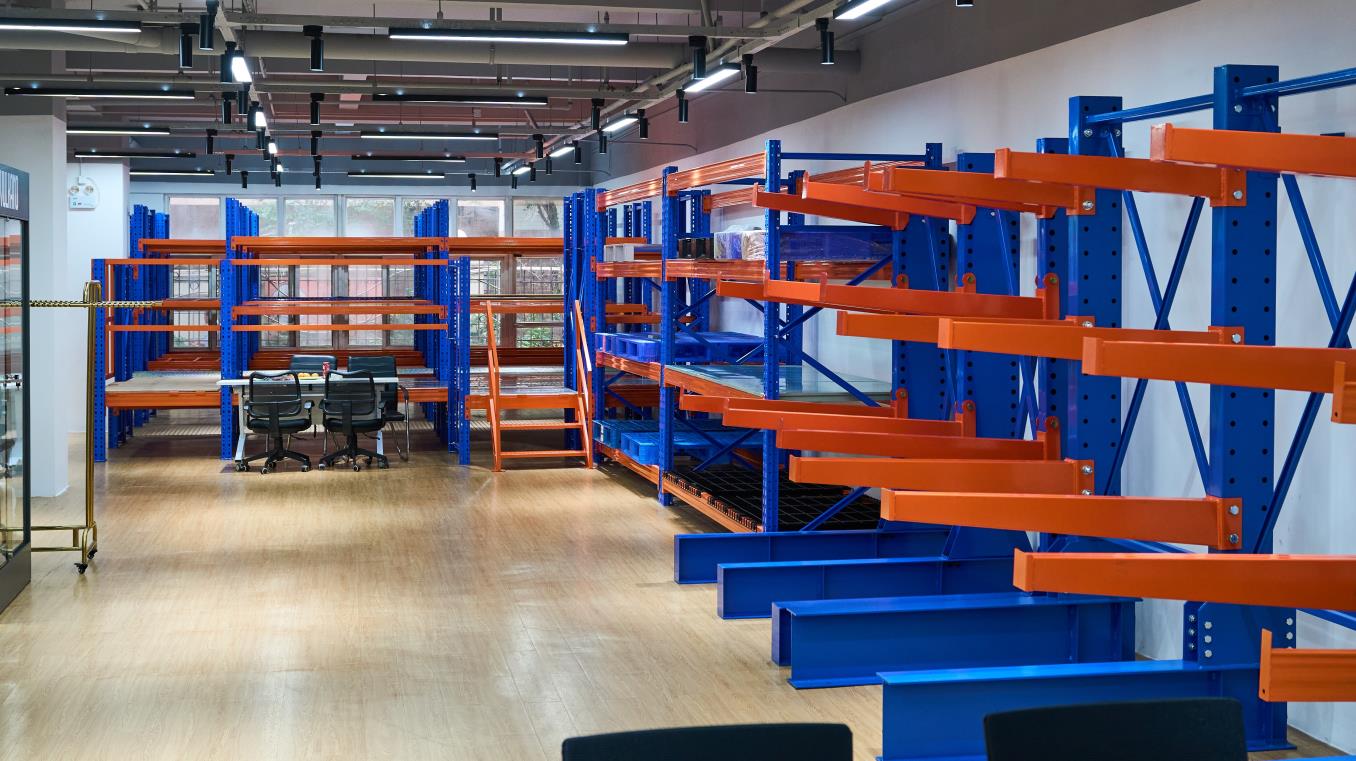
Our R&D capability focuses on High-Density Cantilever & Multi-Tier Mezzanine Engineering. We offer comprehensive custom options ranging from custom RAL color matching and specialized seismic-bracing to specialized rack protectors. Over the past year, we introduced 85 new product launches, developed by our team of 54 R&D engineers.
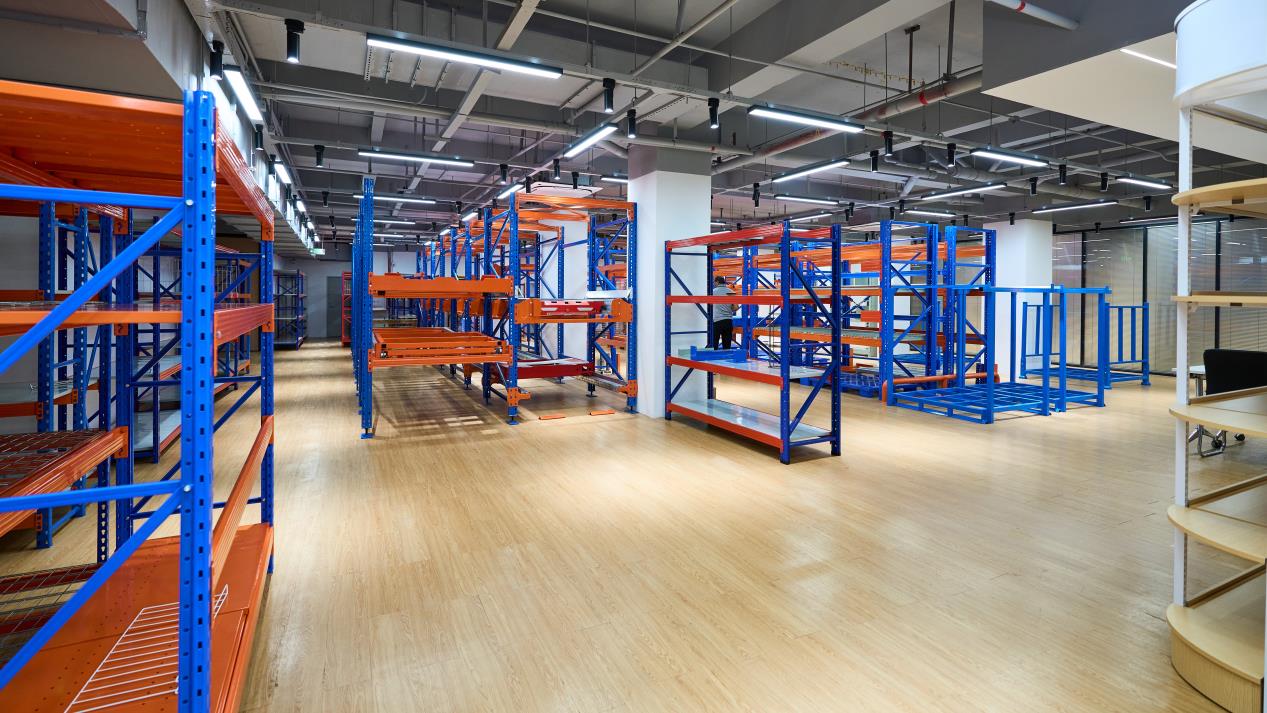
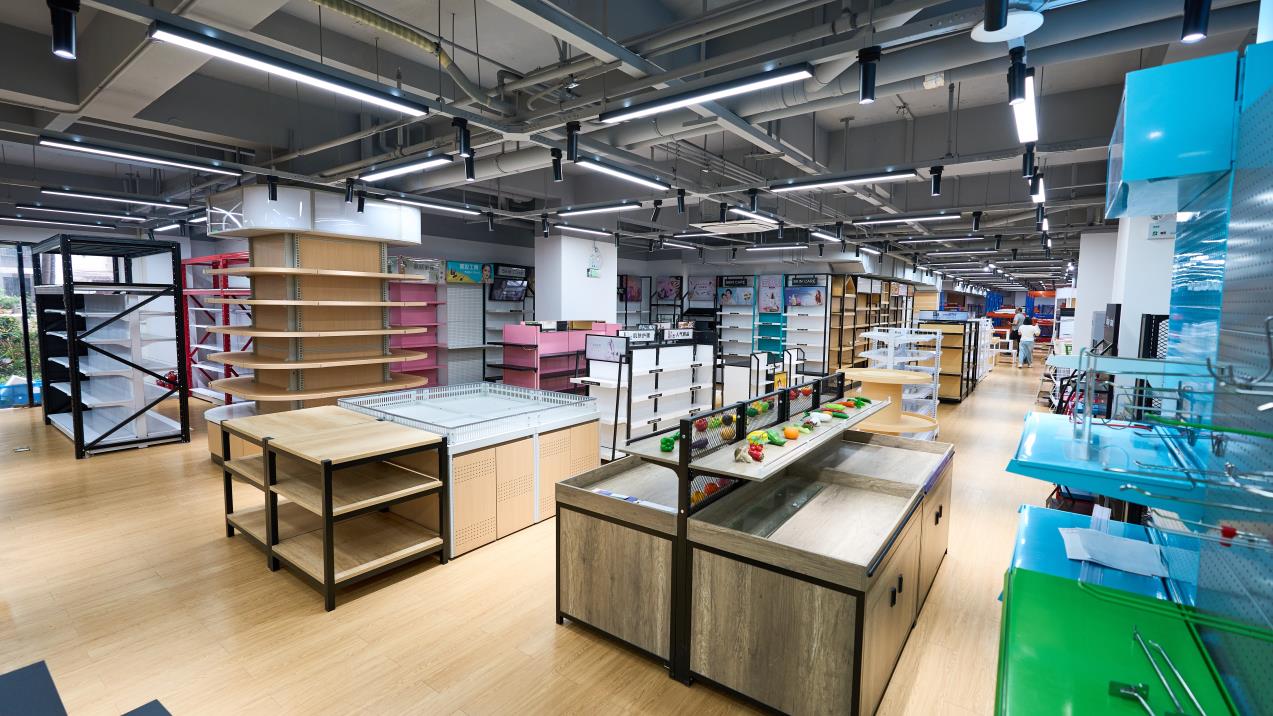
Engineered to adapt seamlessly across diverse operational environments worldwide.
Designed with antimicrobial coatings and cleanroom compliance, our specialized medical cabinetry and pharmacy shelving ensure secure, organized storage for temperature-sensitive drugs, surgical tools, and Western medicine inventories across clinical distribution hubs.
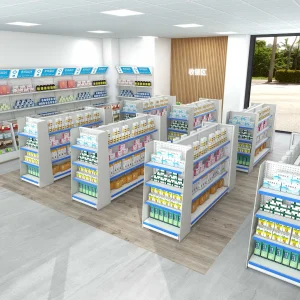
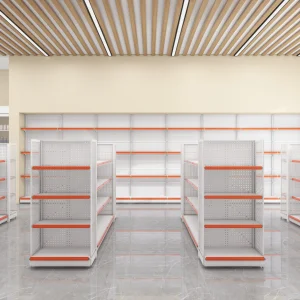
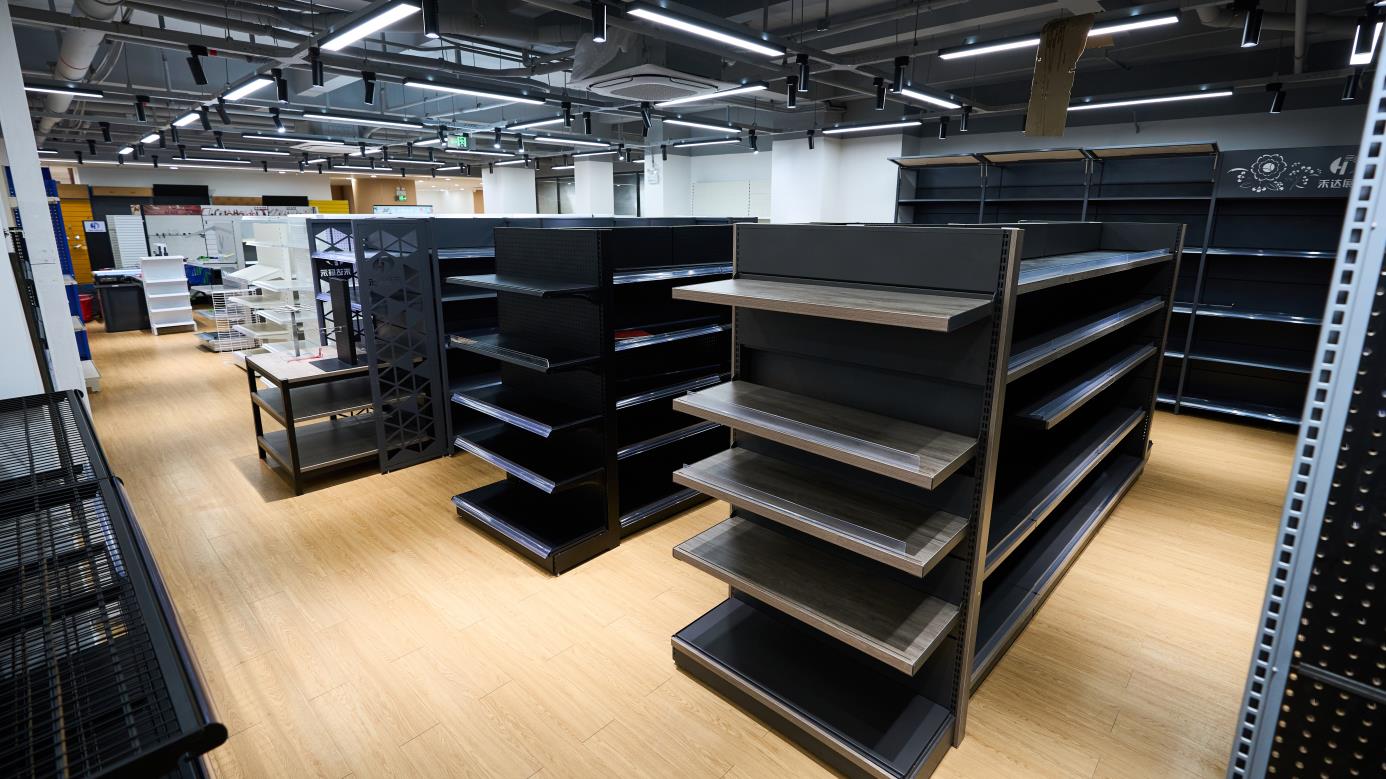
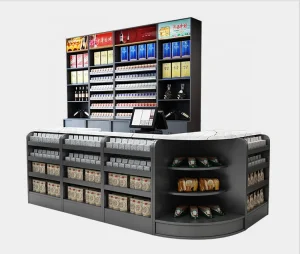
From heavy-duty gondola shelving to customized island display racks and checkout counter sets, our retail storage systems enhance product visibility, maximize floor space utilization, and elevate the customer shopping experience.
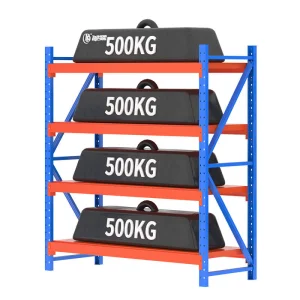
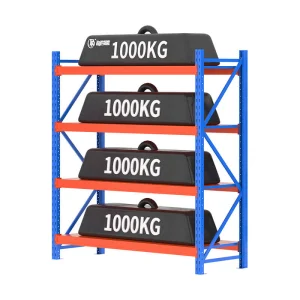
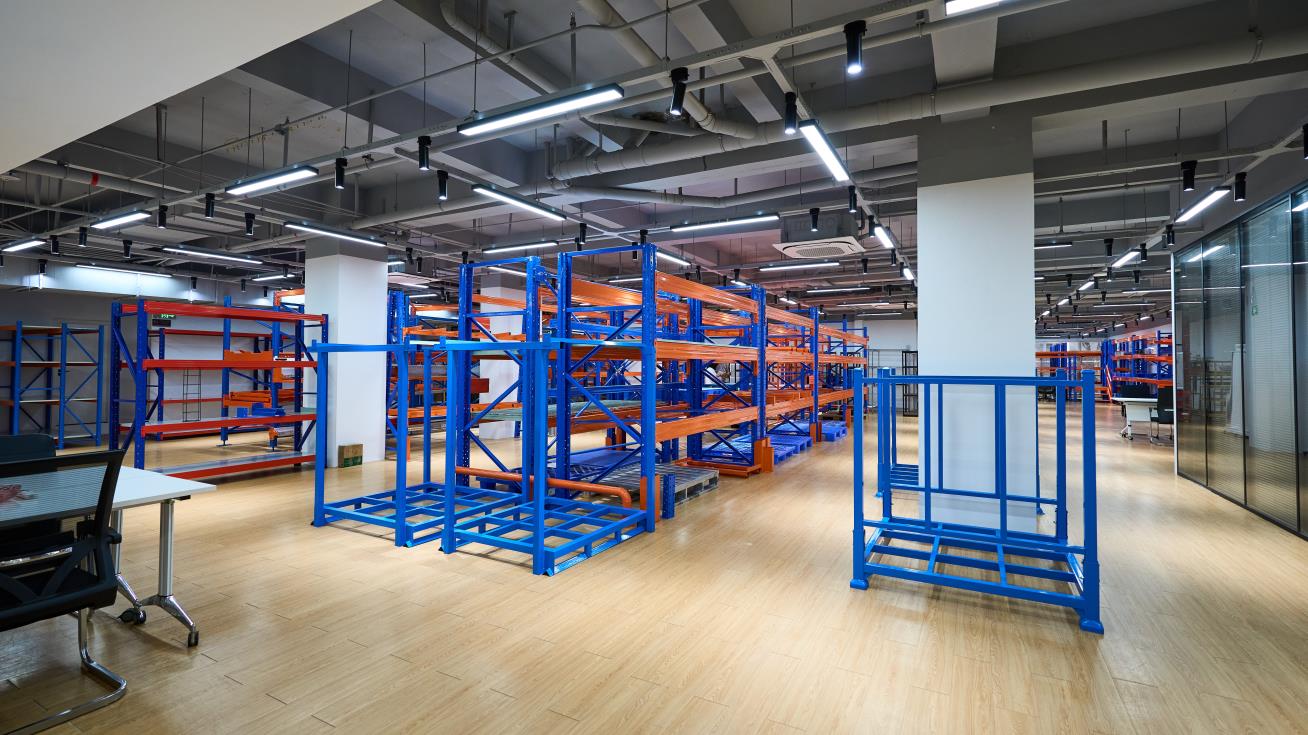
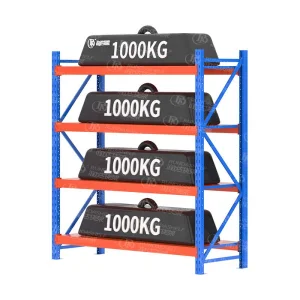
Built for extreme weight capacities (500kg+ per tier) and equipped with automated rollout cantilever racks, our industrial storage systems safely organize steel pipes, raw metals, and bulky palletized goods under rigorous industrial conditions.
Expert answers regarding custom OEM manufacturing, load ratings, and global logistics.
Browse our additional industrial racking systems and multi-tier warehouse platforms.
 CrownRacking